
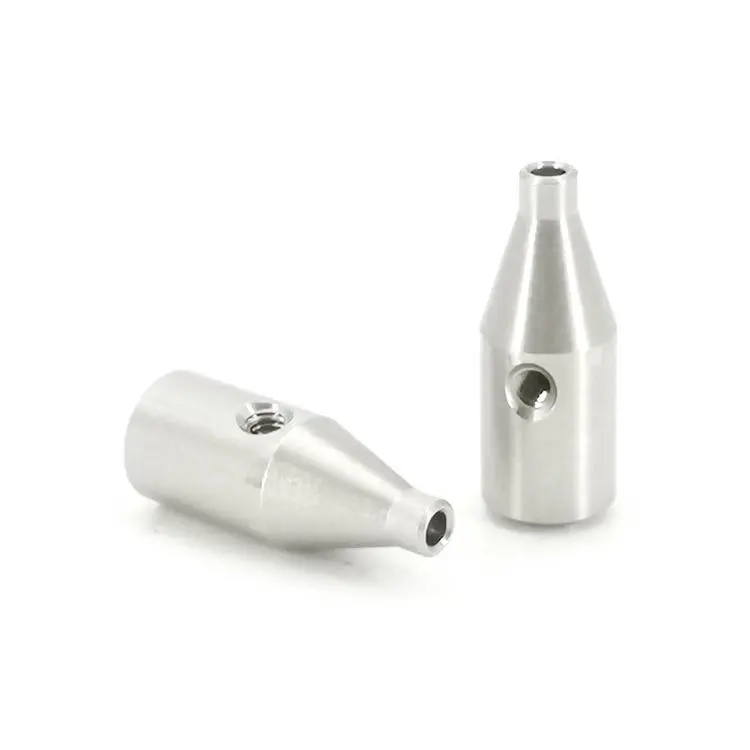
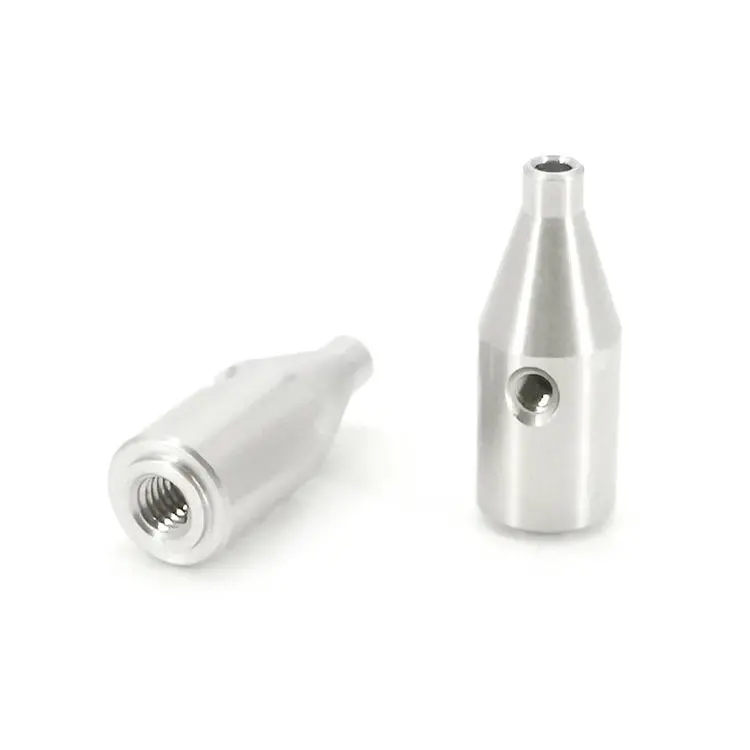
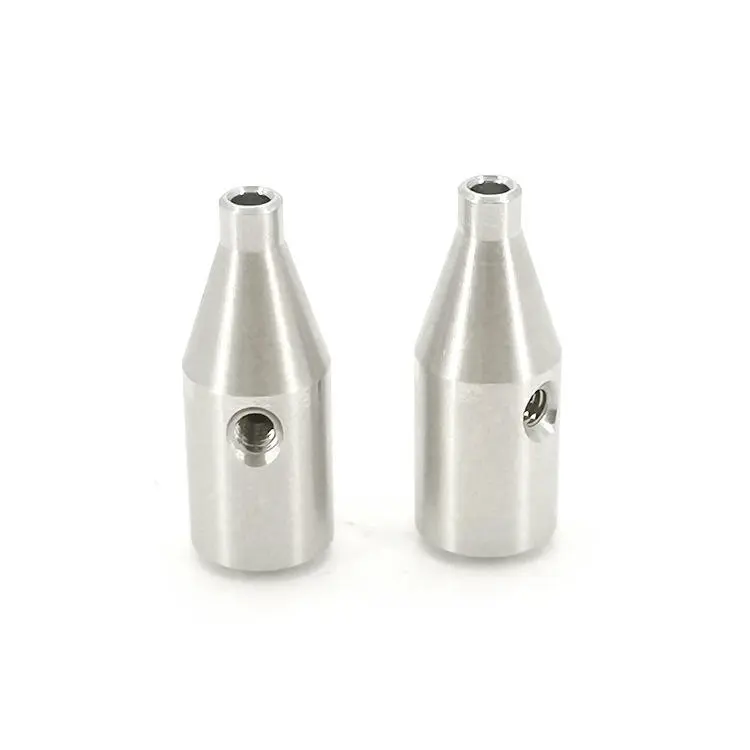
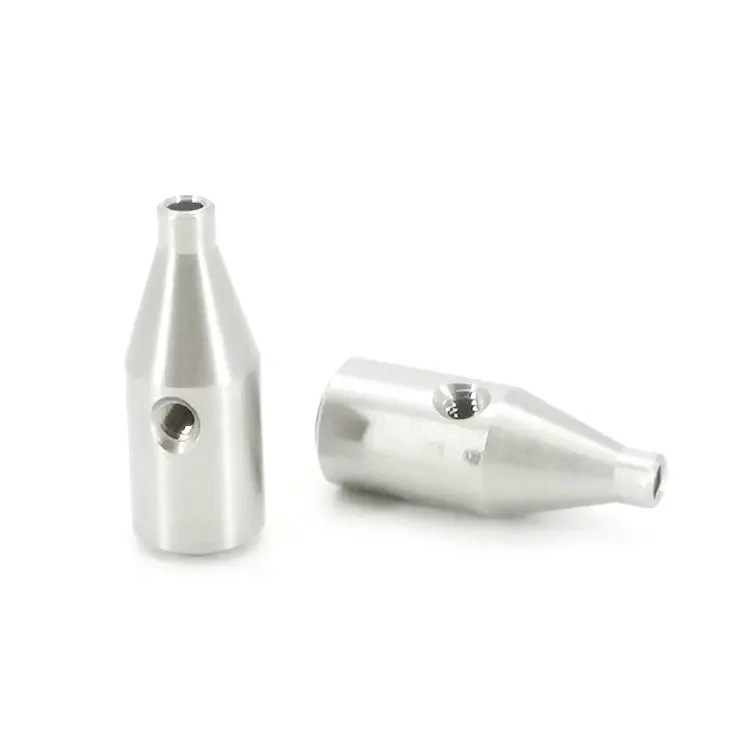
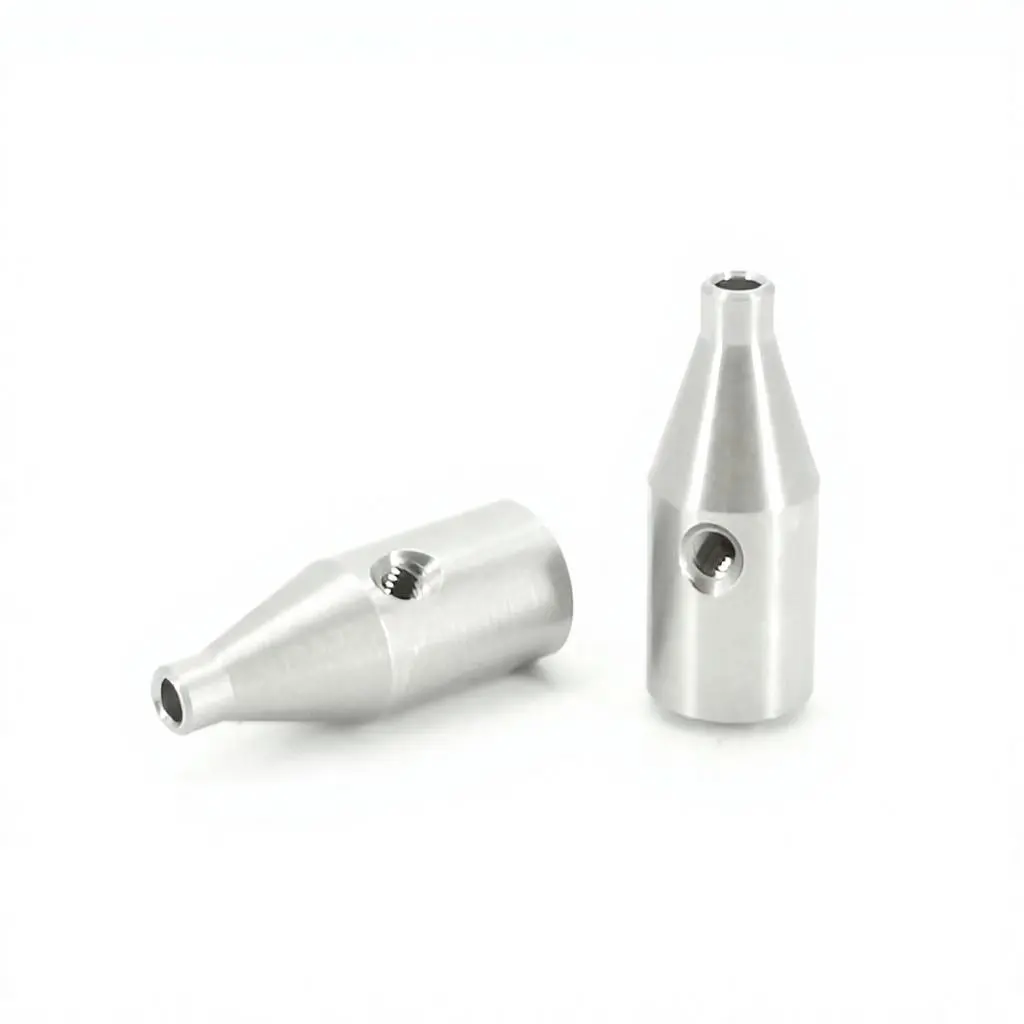
China Custom CNC Turned Aluminum Nozzle & Adapter Bodies Exporter, Factory
Product Description
Product Overview
Fit the component to your instrument, not your instrument to a catalog part. Shenzhen Sunmy Hardware Co., Ltd. manufactures custom aluminum nozzle and adapter bodies from drawings or samples. Tailor the taper, bores, axial thread and radial feature to your mating components and available space. Intended applications include laboratory instruments, analytical equipment and IVD handling systems. For fluid-contact use, define the media, flow path and sealing arrangement. Pressure, flow performance and medical-device suitability require application-specific validation.
Manufacturing & Process Insights
Select CNC turning, side-feature machining, deburring and finishing around your geometry, material and quantity, using one approved drawing and inspection plan:
Datum-Based CNC Turning
Machine tapers, diameters, bores and threads from agreed references. Combine operations where practical and verify the specified datum relationships; a single setup alone does not prove geometric accuracy.
Radial Hole & Thread Machining
Use live tooling or a located secondary setup. Define side-hole position, depth, thread and lead-in geometry, including whether the feature is for fastening or fluid connection.
Cross-Hole Deburring & Cleaning
Control burrs at bore intersections and thread exits. Select deburring, flushing and ultrasonic degreasing for the geometry and material, with residue limits and verification agreed for controlled-cleanliness work.
Surface Treatment & Fit Control
Select the finish for the alloy and application. Define coating thickness, masking and final bore/thread dimensions before machining; available finish options are listed below.
Key Technical Specifications
| Parameter | Specification / Review Basis | Custom Options & Confirmation |
|---|---|---|
| Primary Material | Aluminum 6061-T6 / 6082-T6 / 7075-T6; grade and condition per order. | Stainless steel 303/304/316L, brass, PEEK or POM; application-specific. |
| Manufacturing Process | CNC turning, drilling, boring and internal threading. | Live tooling, secondary milling or Swiss-type machining as appropriate. |
| Dimensional Tolerances | ±0.005–±0.01 mm reference targets; feasibility confirmed per feature. | ISO 2768-1 m/f for untoleranced dimensions only where specified. |
| Geometric Controls | Specify bore location, circular/total runout and datum references. | ≤0.01 mm runout is a reference target, not a universal guarantee. |
| Surface Roughness (Ra) | Ra 0.4–0.8 μm reference targets on identified machined surfaces. | Ra 0.2 μm subject to access and process review; final condition specified. |
| Threaded Interfaces | Metric (M3–M16 examples), UNC/UNF, NPT or BSPP. | Other sizes by drawing; define pitch, class/gauging, depth and sealing. |
| Surface Finishing | Cleaned, bead-blasted, or Type II clear/color anodized. | Type III hardcoat, electroless nickel or chemical conversion; specify masking. |
| Cleaning & Packaging | Degreasing, bore flushing and drying to agreed limits. | Ultrasonic cleaning and protective packaging per cleanliness specification. |
| Quality Control & Records | Thread gauges, optical/CMM checks and bore gauging as appropriate. | Sampling/100% checks and FAI, material or finish reports as agreed. |
| Production Volumes & MOQ | Prototypes, pilot batches and repeat production. | Quantity, MOQ and delivery confirmed with each quotation. |
Key Engineering Advantages & Capabilities
-
Built Around Your Assembly: Customize body and tip diameters, length, taper, bores and threaded interfaces. Reference sizes do not restrict the configurations we can review.
-
Critical Fits First: Identify locating diameters, thread requirements and sealing features. Separate dimensional, geometric and roughness requirements so quotations cover the same acceptance scope.
-
DFM & Prototype Support: Review tool access, bore intersections, thread depth and finishing allowances before machining. Approve samples and drawing revisions before repeat production.
-
Application-Specific Cleanliness: Specify the fluid, cleanliness limits and protective packaging. Material selection alone does not establish suitability for a fluid-contact or laboratory application.
-
Order-Specific Verification: Agree inspection methods, sampling and material or finish records before production. Requested reports and additional tests are included in the quoted supply scope.
Other Products
Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.
Technical FAQ (B2B Buyer Guide)
A: Yes. Send a STEP, IGES or SolidWorks model and a dimensioned PDF, DWG or DXF drawing. Sample-based development is also available with drawing approval before production. Include mating-part details, material, finish and quantity for a project-specific review and quotation.
A: The plan can include calibrated internal-thread plug gauges, optical/CMM measurements, bore gauging and datum-based runout checks. Burr inspection is selected for the available access. Agree sampling, limits and reports before production; leak and cleanliness tests are separate requirements.
A: Indicative ranges are 5–7 business days for prototypes and 15–22 for repeat batches, subject to drawing approval, materials, quantity, finishing and inspection. Send your required quantity and delivery date; the quotation confirms timing and any minimum batch requirement.
A: Yes. Request material certificates, first article inspection (FAI) reports and applicable finish records with the RFQ. Documentation and traceability are agreed before production. Identify dimensions requiring final-finish inspection and any additional cleanliness or application-validation requirements.
A: Finishing options include cleaned, bead-blasted, Type II clear or color anodizing, Type III hardcoat, electroless nickel, and chemical conversion. Coating thickness, masking areas, and final bore/thread dimensions are defined prior to machining to ensure proper assembly fit.
A: Intended applications include laboratory instruments, analytical equipment, and IVD (in vitro diagnostics) handling systems. When used for fluid contact, clients should specify media compatibility, flow paths, and sealing requirements for application-specific validation.









