
Custom Custom Self-Tapping Threaded Inserts Product, Exporters
Product Description
Product Overview
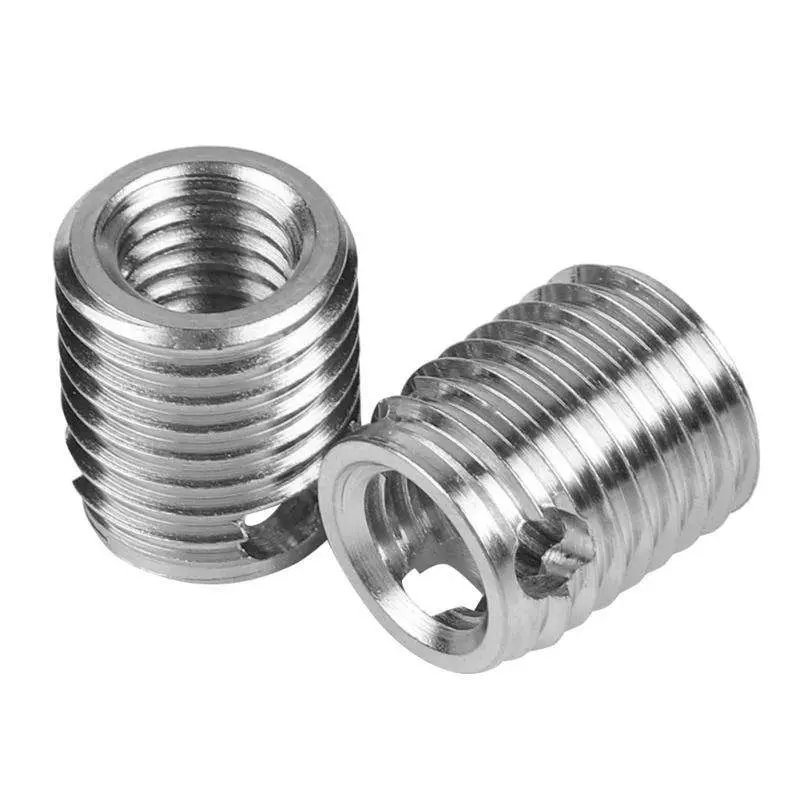
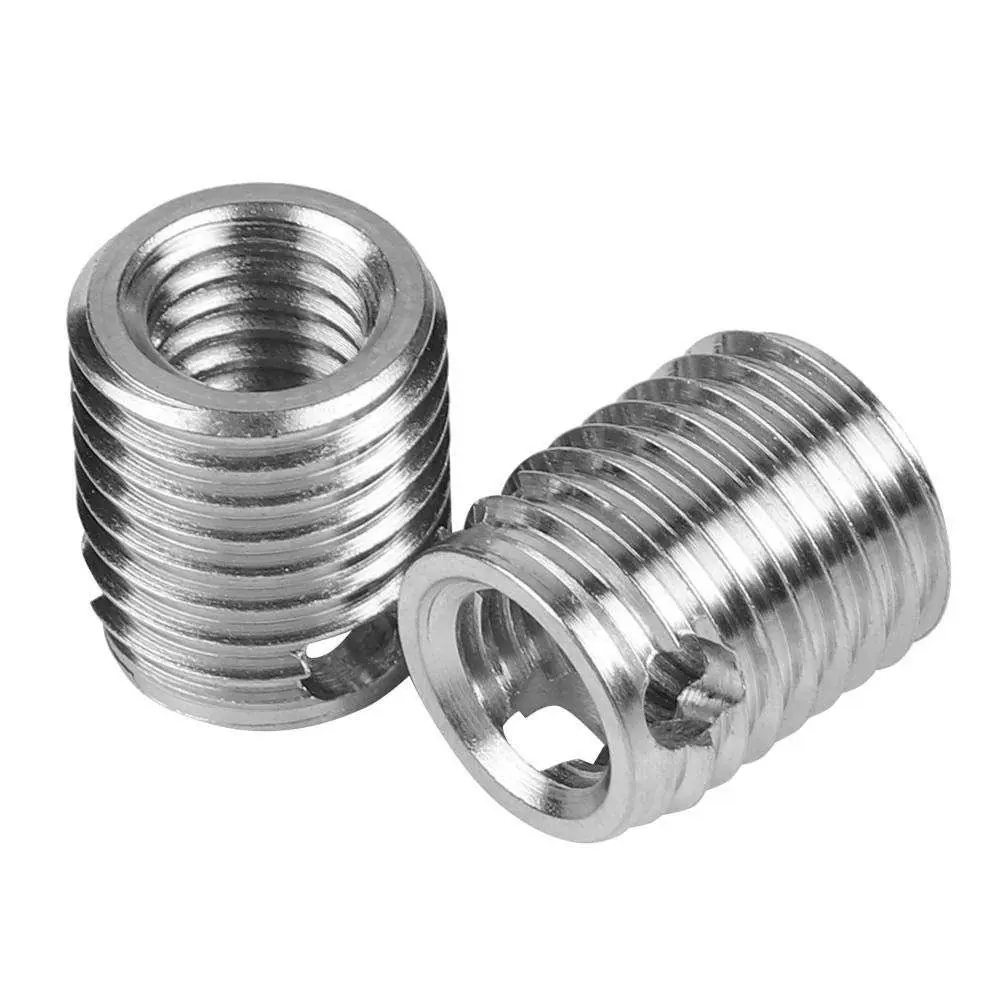
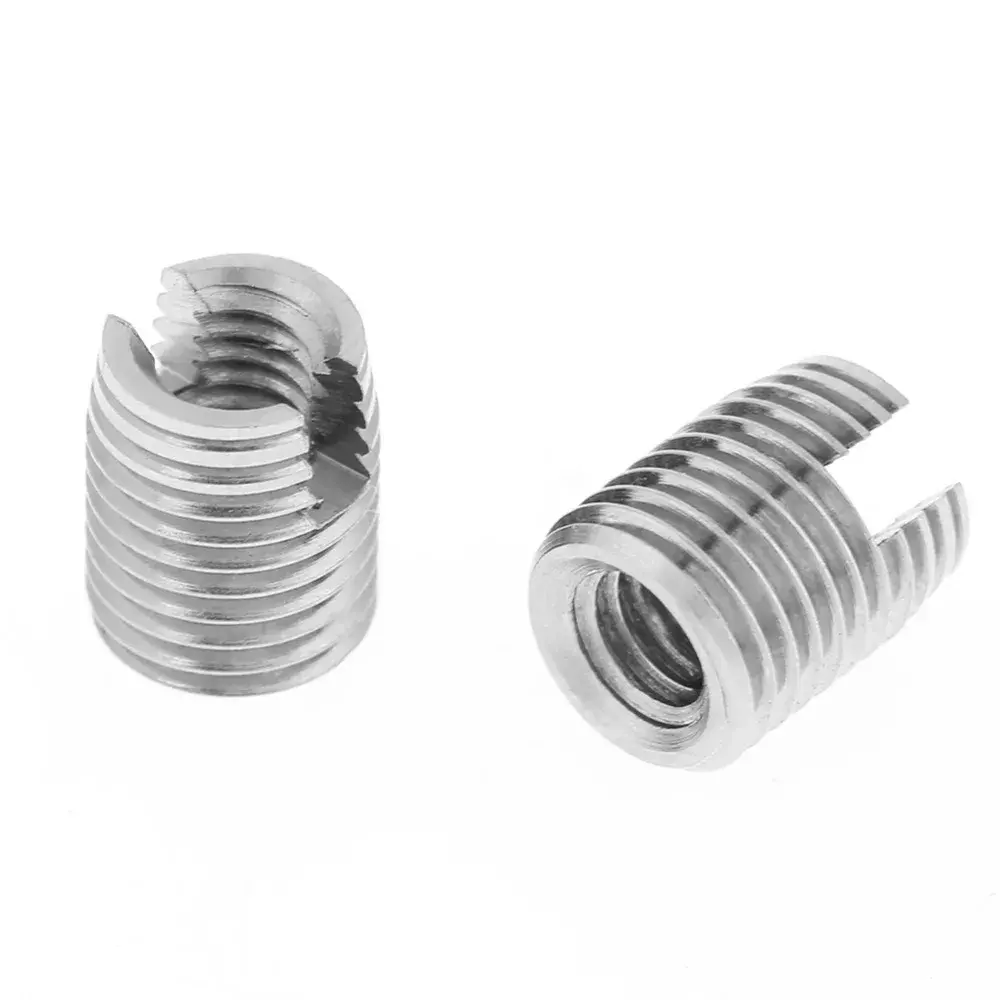
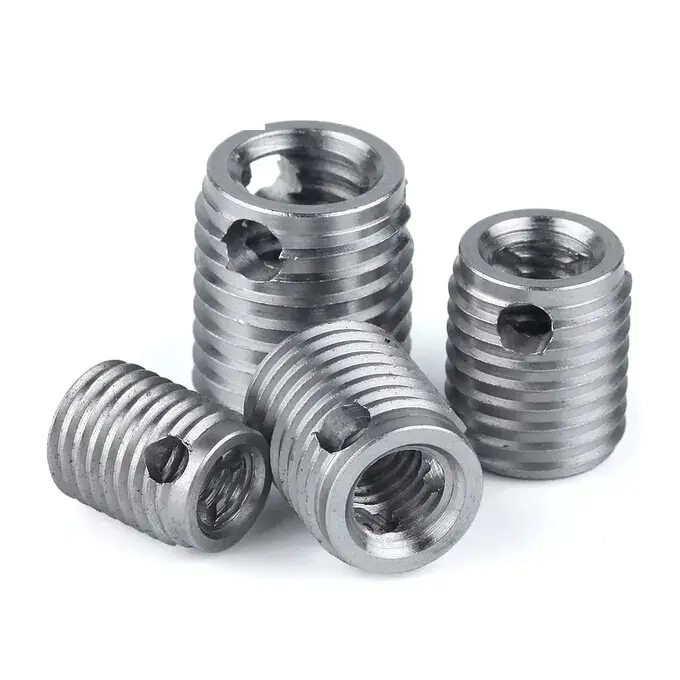
Sunmy manufactures custom self-tapping threaded inserts to your drawings or approved samples. Slotted and three-hole cutting designs can be supplied separately or installed in matching housings. Threads, dimensions, material and finish are tailored to your assembly. A separate tapping operation can be eliminated in suitable applications, with the host material, pilot hole and installation method validated together.
Process & Manufacturing Insights
Shenzhen Sunmy Hardware Co., Ltd. combines CNC turning, threading, milling and drilling to suit your design and production volume:
CNC Turning & Threading
Diameters, bores and chamfers follow your drawing. Internal threads are tapped or single-point cut; external cutting threads follow the specified profile.
Cutting Slots & Radial Bores
Slots and cutting holes are machined to the drawing. Controlled deburring preserves cutting geometry and removes loose chips from the internal thread.
Heat Treatment & Finishing
Hardening is selected for the alloy and cutting duty. Plating or passivation follows your specification, including thread allowance for coating thickness.
Coordinated Parts & Assembly
Casting, turning, CNC machining, stamping and injection molding support matching components. Optional insert installation and assembly checks are defined with your team.
Key Technical Specifications
Made to customer drawings or approved samples. Final specifications and inspection requirements are agreed before production.
| Attribute | Specification Details |
|---|---|
| Product Name | Custom Self-Tapping Threaded Inserts (Slotted & Three-Hole Cutting Types) |
| Material Options | Carbon/alloy steel, suitable stainless steel or brass; grade and condition selected for the application. |
| Structural Design | Slotted cutting end or three radial cutting holes; geometry to the approved drawing. |
| Thread Specification | Internal ISO metric, UNC/UNF or specified thread; external cutting-thread profile defined separately. |
| Size & Geometry | Custom diameters, pitch, length, wall thickness and lead-in; feasibility reviewed before quotation. |
| Dimensional Tolerance | Drawing-specific dimensions and thread classes; critical fits and gauges agreed during review. |
| Surface Treatment | Specified zinc, zinc-nickel or nickel plating; passivation or black oxide where suitable for the alloy. |
| Host Materials | Aluminum/magnesium alloys, cast iron and selected engineering plastics; validate the insert/host combination. |
| Applications | Equipment housings, cast components, machinery, electronics and suitable thread-repair projects. |
| Quality Control | Thread gauging, dimensional and visual checks; material, hardness and finish verification as specified. |
| Customization & Assembly | OEM/ODM, DFM, matching component manufacture and optional insert installation or subassembly. |
| Packaging | Protective bags or trays, batch identification and export cartons; custom packing to order. |
Key Features & Sunmy Advantages
- Built Around Your Design: Custom thread combinations, body lengths and cutting geometry remove the need to redesign your component around a fixed catalogue size.
- Thread Reinforcement: A metal internal thread supports repeated screw assembly in suitable hosts. Retention and torque requirements are validated for the actual joint.
- Installation-Focused DFM: Review pilot-hole size, remaining wall thickness, blind-hole depth and chip clearance before committing to production.
- One Source for the Assembly: Combine inserts, cast or machined housings, molded parts and specified hardware under one coordinated manufacturing and assembly scope.
- Prototype to Repeat Orders: Trial quantities support fit and installation checks. Approved drawings, agreed inspection plans and batch identification support consistent repeat supply.
Related Products
Custom Titanium Ultrasonic Booster
Custom CNC Turned Tooling Sleeves & Threaded Retaining Plugs
Custom Hollow-Shaft Cycloidal Reducer | OEM Parts & Assembly
Custom 6-Axis Force/Torque Sensor Housings & Elastic Elements
Technical FAQ
Slotted designs suit many general applications; three-hole designs can suit more demanding cutting conditions. Selection also depends on host hardness, wall thickness and hole depth. Confirm the pilot hole and insertion method through application trials.
Yes. Threads, dimensions, cutting features, material and finish are customizable. We can also manufacture matching housings and supply installed inserts or assembled components to an agreed specification. Send drawings or samples for review.
Internal threads are gauged; external cutting profiles and dimensions are checked against the drawing. Installation trials, torque and pull-out tests can be specified in the actual host material. Inspection scope is agreed before production.
Prototype, pilot and repeat orders are supported. MOQ and lead time depend on material, geometry, finish and assembly. Send drawings, host-material details, quantity and delivery target for DFM review and quotation.
Self-tapping inserts provide dependable pull-out resistance in aluminum and magnesium alloys, cast iron, and select engineering plastics. Pilot hole diameter, countersink depth, and wall thickness must be validated during DFM review.
Plating thickness allowances (e.g., zinc, zinc-nickel, passivation) are pre-calculated before machining. Both internal thread gauging and external cutting geometries remain strictly compliant with specified drawing classes after finishing.
Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.









