
High-Quality Custom CNC Machined Robotic Gripper Jaws Service, Quotes
Product Description
Product Overview
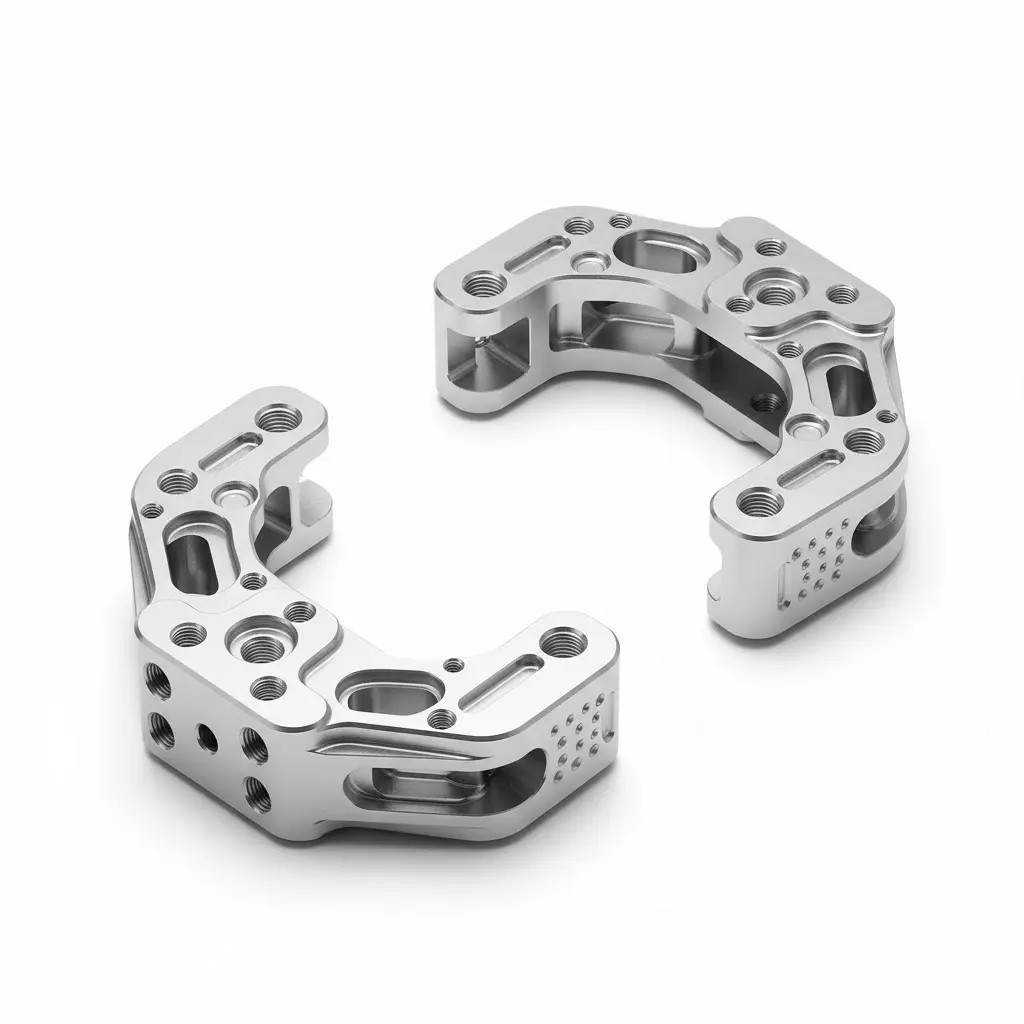
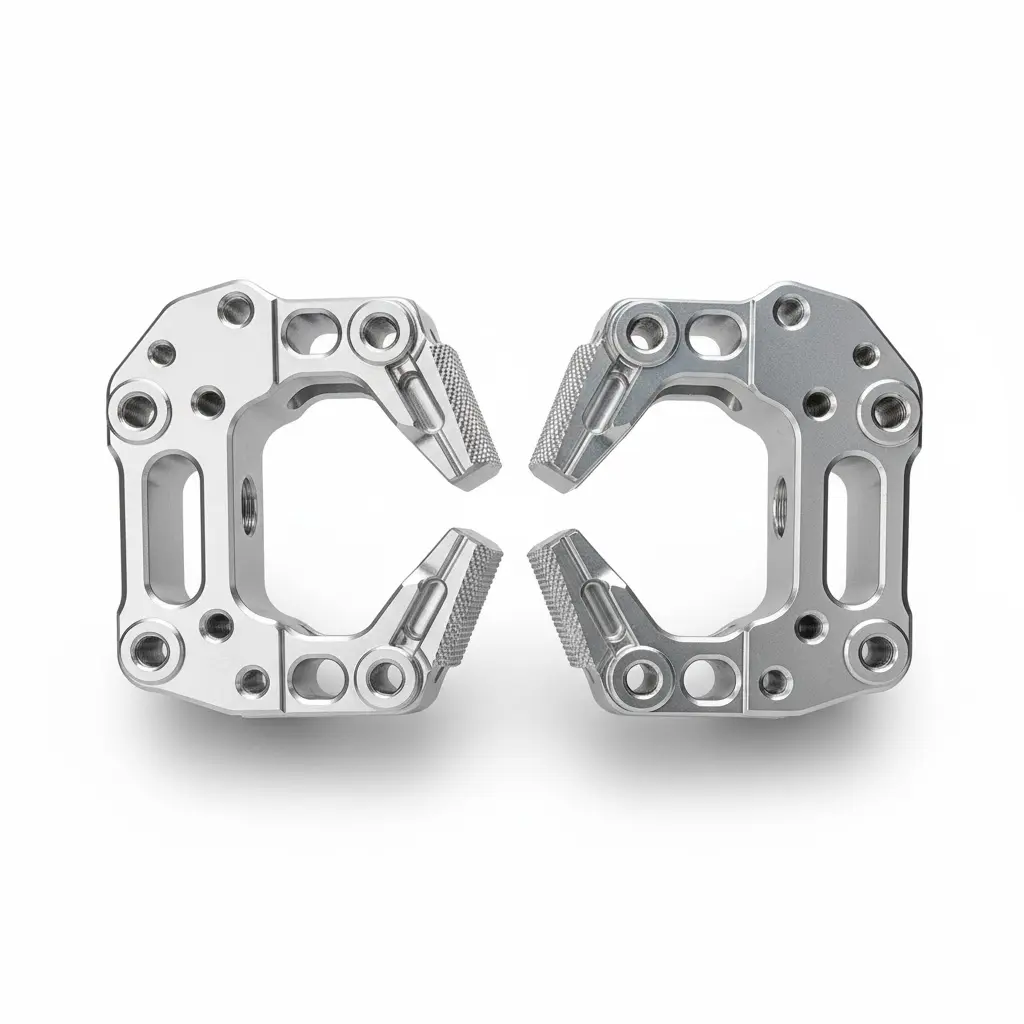
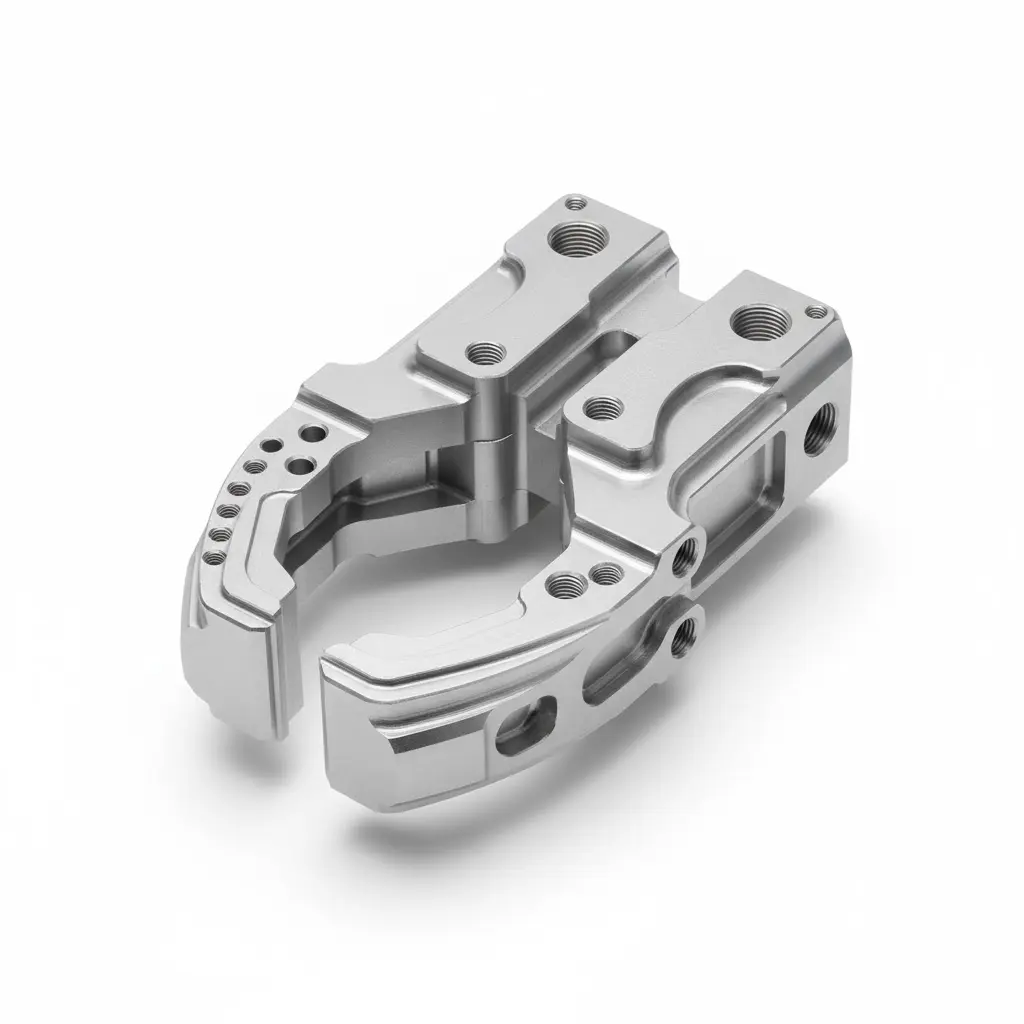
Reliable robotic handling starts at the contact point. Sunmy supplies custom CNC-machined gripper jaws and end-effector components for automated assembly, machine tending and pick-and-place systems. Features such as threaded mounting interfaces, relief pockets, locating holes and contoured gripping faces are manufactured to customer drawings. Our team reviews material choice, critical fits and manufacturability before moving from a prototype to repeat production.
Manufacturing & Process Insights
3-, 4- and 5-axis strategies are selected to suit the geometry. Datum control, access to deep pockets and the relationship between mounting holes and gripping surfaces are reviewed before machining.
Pocketing can reduce moving mass, but thin walls, corner radii and load paths must be checked against the required grip force and robot acceleration. Material is removed where it makes engineering sense.
We machine custom slots, tapped holes, dowel locations and contact profiles. Serrations or replaceable grip pads can be evaluated when handling delicate, smooth or irregular workpieces.
Bead blasting and clear, black or hard anodizing are options for aluminum; passivation and other suitable finishes can be specified for stainless steel. Coating thickness and mating surfaces are considered in the machining plan.
Technical Specifications
| Parameter | Specification / Capability | Customer Customization Options |
|---|---|---|
| Product Name | Custom CNC-Machined Robotic Gripper Jaws | Made to your 2D drawings, 3D CAD or approved samples |
| Manufacturing Processes | CNC milling (3/4/5-axis); CNC turning and EDM where needed | Process and setup selected to suit geometry and volume |
| Material Options | Aluminum 6061-T6 / 7075-T6; stainless 304 / 316L / 17-4PH; POM / PEEK | Other material grades considered after application review |
| Dimensional Tolerances | Defined by the drawing, feature geometry and intended fit | Critical GD&T and achievable limits confirmed during DFM |
| Surface Roughness | Machined finish; specified Ra values on functional surfaces | Target finish and inspection method agreed per feature |
| Surface Treatments | Bead blasting; clear/black/hard anodizing; passivation; nickel plating | Finish selected for wear, corrosion and mating requirements |
| Mounting Features | Tapped holes, counterbores, dowel bores, slots and grip profiles | Metric or imperial interfaces to your actuator design |
| Quality & Inspection | CMM, optical measurement, thread gauges and dimensional checks as applicable | FAI, material certificates or detailed reports by agreement |
| Quality Management | ISO 9001 quality management system | Traceability and application-specific documentation as agreed |
| Accepted Drawings | STEP, PDF, DXF, DWG, IGES; other CAD formats by arrangement | NDA and DFM review available before manufacturing |
| Order Quantity & Lead Time | One-off prototypes, pilot batches and repeat production | Lead time confirmed after drawings, volume and finish review |
Key Features & Sunmy Manufacturing Advantages
Hole patterns, datums, jaw profiles and fastening features follow your CAD rather than a generic catalogue size.
Lightweight pockets, contact geometry and alloy selection are assessed against stiffness, grip force and cycle requirements.
Critical bores, locating features and threaded interfaces can be checked to an agreed inspection plan before shipment.
Sunmy supports CNC, casting, stamping and injection molding when a revised design or higher-volume program makes another process viable.
Other products
Technical FAQ for International Buyers
Yes. Send a STEP model and any critical 2D dimensions. We can review tool access, thin sections, locating features, material options and cost drivers, then flag questions before quotation.
Inspection is planned around the drawing datums and critical characteristics. Depending on the features, we use CMM measurement, gauges and dimensional checks. FAI or additional reporting can be agreed with the order.
Yes. We support initial samples, low-volume builds and repeat production. Quoted price and lead time depend on geometry, quantity, tolerances and finishing. Send your drawing and target volume for a practical proposal.
We accept native STEP, IGES, PDF, DXF, and DWG files. For 3D geometries, STEP files are preferred along with a 2D PDF specifying critical GD&T and thread requirements.
Coating thickness is factored into the pre-machining dimensions. For critical dowel holes and sliding interfaces, surfaces can be masked or post-machined to ensure specified tolerance adherence.
Aluminum 6061-T6 and 7075-T6 are widely chosen for high strength-to-weight ratios. For non-marking or electrically insulative applications, engineering plastics like POM or PEEK are readily machined.
Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.









