
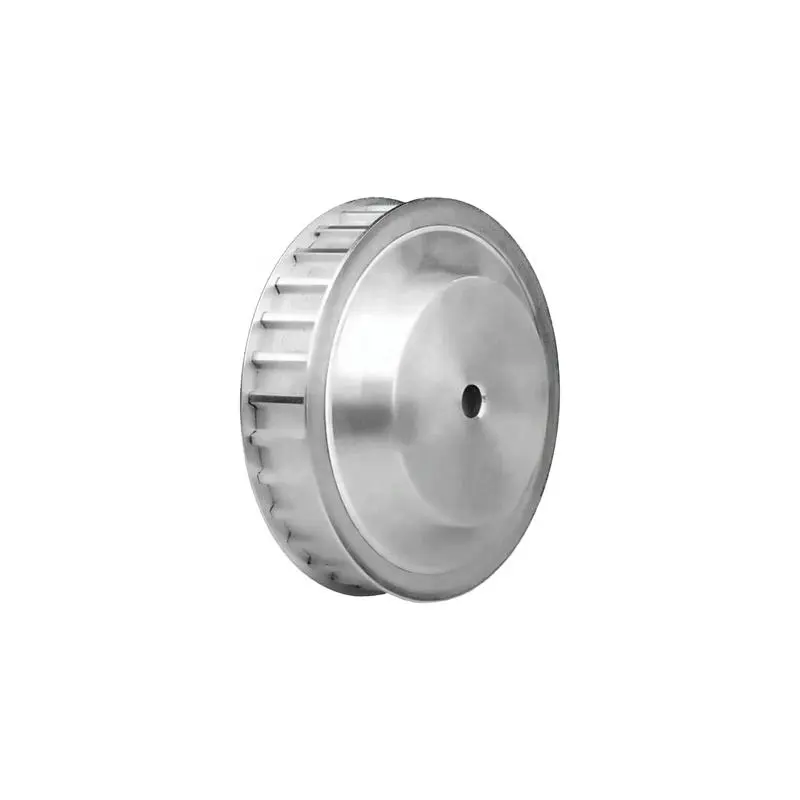
OEM Custom CNC Machined HTD 3M Aluminum Timing Belt Pulley Supplier, Products
Product Description
Product Overview & Engineering Scope
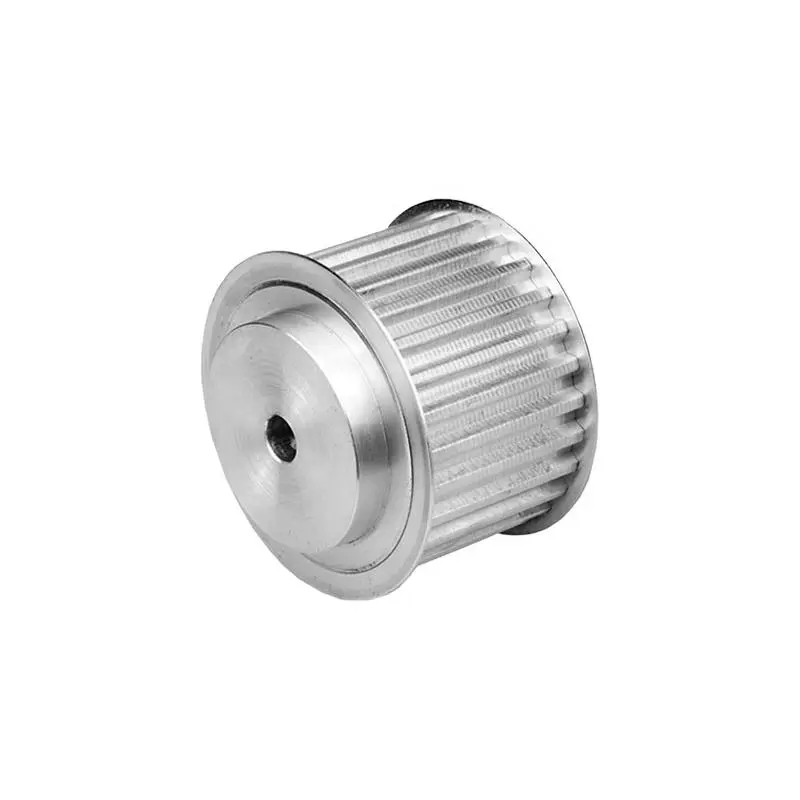
Shenzhen Sunmy Hardware Co., Ltd. manufactures custom aluminum timing pulleys from customer drawings, CAD models or approved samples. HTD 3M-15 identifies the reference configuration: 3.00 mm pitch for a nominal 15 mm HTD 3M belt. Tooth count, face width, bore, hub, flanges, material and finish can all be customized. Confirm the exact mating belt profile before production; matching pitch alone is insufficient.
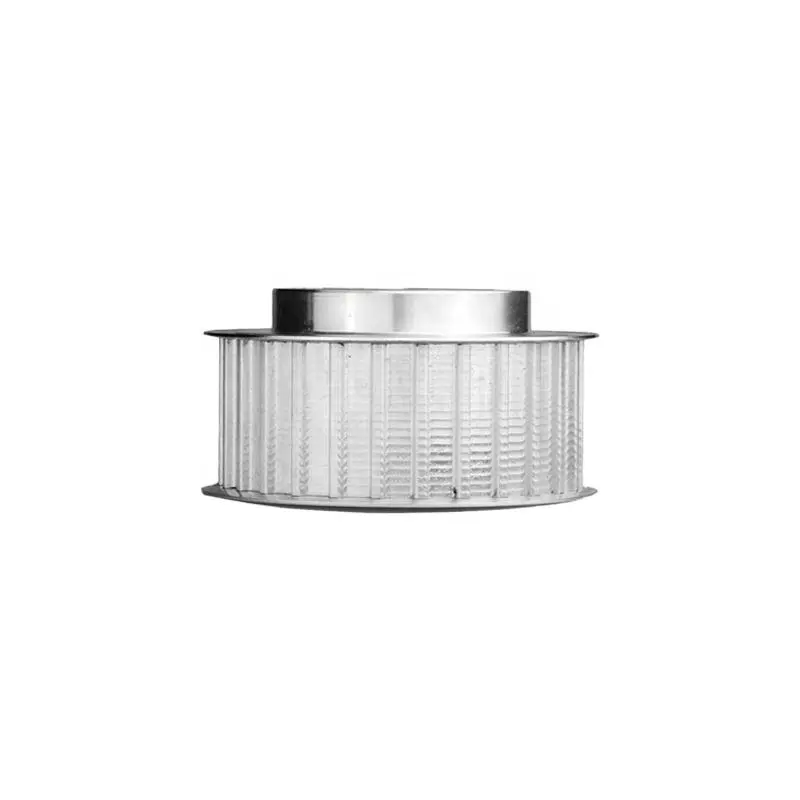
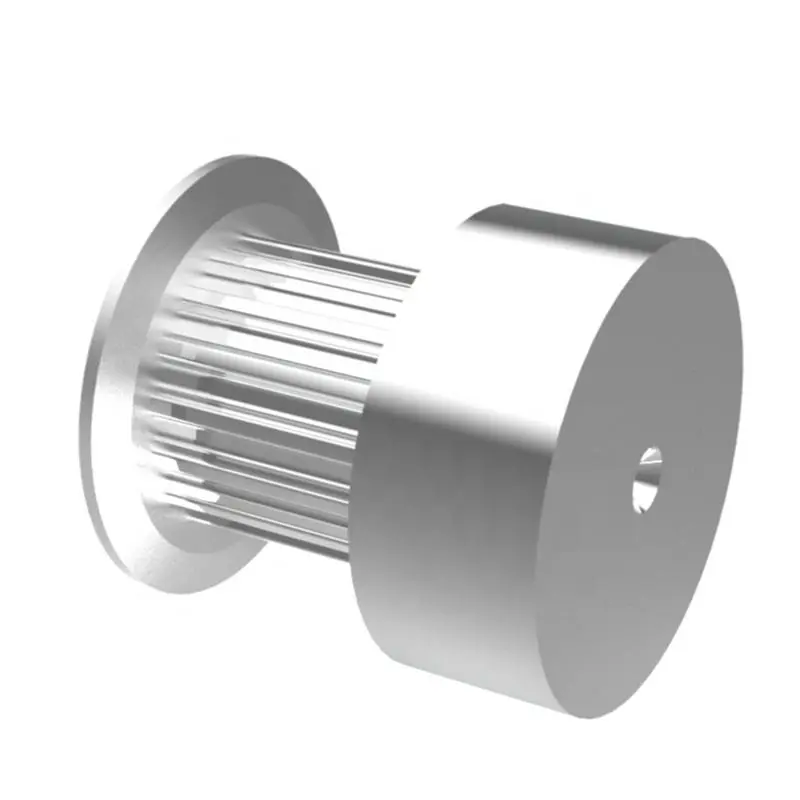
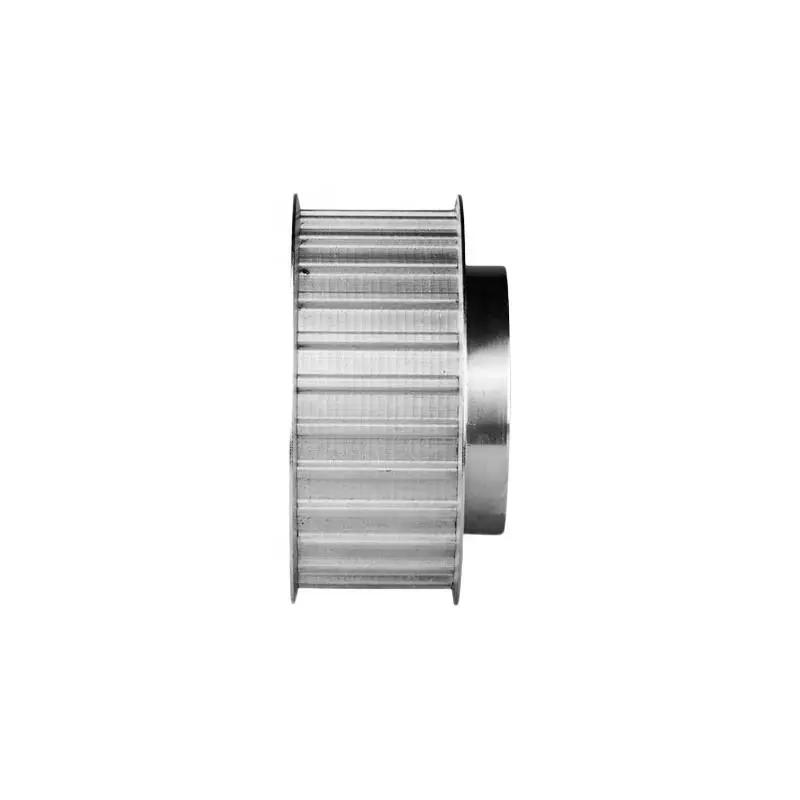
Material options include 6061-T6 and 7075-T6 aluminum, with grade and temper specified per order. Reference sizes are neither catalog limits nor a stock guarantee. Pilot bores, finished bores, keys, D-bores, set-screw holes and split-clamp hubs can be evaluated. Photographs show example configurations; the approved drawing defines the supplied geometry and finish.
Application Areas: Custom components evaluated against the equipment requirements.
Process & Manufacturing Insights
The following steps describe available manufacturing and inspection operations. Sunmy coordinates the selected route, process sequence and quality requirements for the approved design and production quantity.
Material Selection & Blank Prep
Confirm alloy, temper, stock form and required material records. Select roughing allowances and any stress-management steps to suit the blank and preserve the specified final material condition. Additional testing is included when required by the material or project specification.
Datum-Controlled CNC Turning
Machine the tooth blank, hub, flange seats and bore from coordinated datums. Use a common setup where practical and transfer the functional bore axis consistently to later operations. Inspection references the final drawing datums and specified radial/axial runout limits.
Matched-Profile Tooth Cutting
Select CNC hobbing or suitable profile cutting for the required tooth geometry and quantity. Match tooling and inspection references to the mating belt; confirm any specified standard and edition. Different belt systems are not assumed interchangeable solely because their pitch matches.
Flange Manufacture & Assembly
Flange material, diameter, thickness and number follow the drawing. Separate flanges may be staked or swaged; integral flanges require suitable machining access. The attachment sequence, retention criteria and testing are defined for the specified flange construction and operating conditions.
Finished Bores & Fastenings
Bore or ream to the required shaft fit. H7 numerical limits depend on nominal bore size, and the resulting fit also depends on the mating shaft. Keyway geometry, set-screw threads and angular positions are defined individually; clamping designs require sufficient hub material.
Deburring & Surface Finishing
Control tooth-edge burrs, bore entries and flange contact edges. Options include clean as-machined surfaces, clear or black anodizing, hard anodizing and selected plating. Specify treatment, coating thickness and masking where needed, with final dimensions checked after finishing as required.
Inspection & Quality Control
Select suitable profile inspection, bore gauges, runout fixtures and coordinate measurement for the critical features. Agree sampling, first-article reporting and material or finish records before production. Balance testing and application trials are separate requirements, not automatic equivalents of dimensional inspection.
Technical Specifications & Customization Matrix
Reference configurations and custom options are shown below. The approved drawing and quotation define the final dimensions, materials, operating requirements and acceptance criteria. Listed sizes do not limit customization.
| Parameter / Attribute | Reference Configuration | Sunmy Custom Capability (OEM/ODM) |
|---|---|---|
| Product Series | HTD 3M-15 reference configuration | Fully custom pulleys to drawings or approved sample specifications |
| Tooth Profile | HTD 3M curvilinear; confirm mating belt | Other profiles to the matching belt drawing; no pitch-only interchangeability |
| Pitch | 3.00 mm (0.118 in) | Other pitches and tooth systems reviewed to the specified belt |
| Compatible Belt Width | 15 mm nominal belt width | Other belt widths with matched tooth face width and flange clearance |
| Face Width & Axial Envelope | Usable tooth width specified separately | Define flange spacing, flange thickness and overall hub-to-face length |
| Tooth Count (Z) | 10T–72T reference options | Other counts subject to belt, hub geometry and tooling review |
| Tooth Outside Diameter (OD) | Defined by tooth count and profile geometry | Specify tooth OD separately from pitch diameter and flange OD |
| Pitch Diameter (PD) | PD = Z × p / π; p = belt pitch | At 3 mm pitch: 10T ≈ 9.55 mm; 72T ≈ 68.75 mm |
| Bore Supply Condition | Unbored blank, pilot bore or finished bore | State required delivery condition; stock blanks are not assumed |
| Finished Bore Options | Size and geometry to the shaft drawing | Round, stepped, keyed, D-bore, spline or clamp interface |
| Bore Fit Tolerance | H7 or explicit dimensional limits as specified | Numerical limits depend on nominal size; review the mating shaft fit |
| Shaft Locking Methods | Selected to shaft and load requirements | Set-screw holes, keyways or split-clamp hubs; hardware scope agreed |
| Hub Configuration | Stepped or single-sided hub by design | Custom height/diameter, double or flush hubs and relief pockets |
| Flange Construction | Flanged or unflanged per drawing | Custom flange material, diameter, number and attachment method |
| Primary Material | Aluminum 6061-T6 / 7075-T6 options | Steel, stainless steel, brass or POM alternatives reviewed on request |
| Surface Treatment | As-machined or customer-selected finish | Clear/black/hard anodizing or suitable plating; final-fit allowance defined |
| Runout & Tooth Finish | Limits and datums defined on the drawing | Agree radial/axial runout, measurement surfaces and roughness requirements |
| Balance & Operating Speed | Operating speed and duty defined per project | Specify service speed, balance criteria, test setup and validation scope |
| Drawing Formats | 2D: PDF, DWG, DXF; 3D: STEP, IGES | Sample-based development with drawing approval before production |
| Quality Documentation | Defined in the order and inspection plan | Dimensional, material, finish and conformance records as agreed |
Key Features & Engineering Advantages
Other Products
Custom Titanium Ultrasonic Booster
Custom CNC Turned Tooling Sleeves & Threaded Retaining Plugs
Custom Hollow-Shaft Cycloidal Reducer | OEM Parts & Assembly
Custom 6-Axis Force/Torque Sensor Housings & Elastic Elements | OEM/ODM
Technical FAQ for International Procurement
Q1: Can Sunmy customize the pulley beyond the reference sizes and bore options?
A: Yes. Tooth count, belt width, bore, keyway, set-screw arrangement, hub geometry, flange construction, material and finish can be manufactured to your requirements. Send the shaft and belt details with drawings or a sample. We review compatibility and manufacturability, then confirm the production drawing before work begins.
Q2: How are prototype and production lead times confirmed?
A: We quote prototypes, dedicated cutting tools, finishing and repeat production separately where relevant. Timing depends on the approved geometry, material availability, tooling, inspection scope and quantity. Provide your target date and trial quantity so we can confirm a realistic schedule and any practical expedited option.
Q3: What information is needed for DFM review and quotation?
A: Send a STEP or IGES model with a dimensioned PDF, DWG or DXF drawing. Include the exact belt profile, pitch, tooth count, belt width, shaft interface, material, finish and quantities. Relevant speed, torque and installation details help define the review. Sample-based development is also supported, with drawings submitted for approval.
Q4: How are tooth accuracy and repeat-order consistency checked?
A: The inspection plan references the approved belt profile and drawing revision. Suitable methods are chosen for tooth geometry, bore fit, radial/axial runout, flange position and surface condition. Sampling and report scope are agreed before production. First-article, material, finish and conformity records are supplied as specified; balance testing is agreed separately.
Q5: Do you support small trial batches and ongoing OEM supply?
A: Yes. Prototype, pilot and repeat-production quantities can be evaluated without forcing a standard catalog size. Minimum practical quantities and price breaks depend on the design, material, tooling and finishing route. Send your drawing or sample details, initial quantity and expected repeat volumes for a project-specific offer.
Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.









