
High-Performance Turned, Machined & Tooling Products
Direct factory export specifications machined to ±0.005 mm tolerances. Fully verified with CMM inspection data and First Article Inspection (FAI) reports before shipment.








Engineering Paradigms in Modern PET & Engineering Plastic Molding
How advanced polymer physics, optical clarity demands, and multi-cavity hot runner systems are reshaping global manufacturing benchmarks.
Polymer Rheology, Crystallinity, and PET Preform Thermodynamics
Polyethylene Terephthalate (PET) and modified engineering PET (such as PETG and fiber-reinforced PET compounds) occupy a unique thermodynamic envelope compared to standard polyolefins. The material exhibits both amorphous optical transparency and high semi-crystalline structural rigidity depending on cooling curves and molecular orientation. In modern injection stretch blow molding (ISBM) and high-speed injection molding tooling, the management of intrinsic viscosity (IV) degradation is critical. Shear heating within the screw barrel and hot runner manifolds can precipitate hydrolytic and thermal degradation, yielding elevated acetaldehyde (AA) levels and molecular chain scission that compromise tensile strength.
As an authoritative ODM Pet Molding exporter, Shenzhen Sunmy Hardware integrates precision tool design with predictive mold-filling analysis. Our tooling engineers utilize Moldflow rheological simulations to map shear stress distribution, gate freeze-off timing, and volumetric shrinkage before cutting steel. For optical housings, consumer preforms, and medical-grade transparent assemblies, cooling channels are CNC-drilled using conformal cooling algorithms or vacuum-brazed copper-beryllium inserts. This achieves rapid heat extraction across critical core pins, mitigating residual stress birefringence and cycle-time bloat.
| Polymer Metric | Standard Virgin PET | High-IV Technical PET | Sunmy Tooling & Process Control Benchmark |
|---|---|---|---|
| Intrinsic Viscosity (IV) | 0.72 – 0.80 dL/g | 0.82 – 0.88 dL/g | Closed-loop desiccant drying dew point < -40°C; IV loss < 0.02 dL/g |
| Glass Transition (Tg) | 67 – 78 °C | 78 – 82 °C | Conformal chiller circuits holding mold surface temp at 8 – 12 °C |
| Acetaldehyde (AA) Content | < 3.0 ppm | < 1.5 ppm | Low-shear valve gate manifolds with individualized tip PID controllers |
| Dimensional Tolerance | ±0.10 mm | ±0.05 mm | Core-cavity alignment held to ±0.005 mm using optical Swiss jig grinding |
Global Procurement Strategy: Overcoming Supply Chain Friction & Total Cost of Ownership
Global procurement teams across Europe, North America, and the Asia-Pacific region are moving away from simple piece-part pricing models toward holistic Total Cost of Ownership (TCO) assessments. When sourcing high-volume PET injection molds and custom precision machined inserts, hidden costs typically surface in three critical zones: premature mold wear, unannounced cavitation imbalances, and lengthy engineering changes (ECN) handled through bureaucratic trading intermediaries.
Sunmy Hardware resolves these procurement bottlenecks through direct factory-to-engineer interaction. By operating owned CNC machining, Swiss turning, and stamping facilities alongside long-term audited casting partners, Sunmy guarantees full transparency. Steel certifications for high-wear cavity inserts (e.g., Stavax ESR, ASSAB S136, H13 hardened to 50–54 HRC) are furnished with metallurgical spectroscopic proofs. The result is mold tooling rated for 1,000,000 to 3,000,000 shots without dimensional drift, drastically lowering cost-per-part over product lifecycles.
Macro-Industry Solutions & Engineered Component Integration
Delivering custom structural integrity, high dielectric isolation, and precision mating surfaces across mission-critical sectors.
Automotive & EV Lightweighting
Structural PET/PBT composite housings, high-voltage connector housings with flame retardancy (UL94 V-0), and precision turned busbar terminal inserts that reduce curb weight while maintaining dielectric isolation up to 1000V.
Medical Diagnostics & Fluidics
Cleanroom-compliant micro-molding for fluidic cassettes, diagnostic reagent vials, and biocompatible medical sleeve bushings. Strict control over flash, particulates, and chemical resistance under rigorous autoclave cycles.
Industrial Robotics & Sensing
Reinforced housings for 6-axis force/torque sensor elements, cable carrier track linkages, and multi-axis joint covers subjected to continuous harmonic vibration and cyclical mechanical loading.
Optical Packaging & Consumer Tech
High-transparency optical barrels, scratch-resistant electronic covers, and RF sensor enclosures combining ultra-high polish (SPI A-1 diamond finish) with EMI/RFI shielding gaskets.
Five Core Capabilities Coordinated Under One Direct Facility
Owned CNC milling and stamping plants paired with certified casting and molding infrastructure in Shenzhen, China.
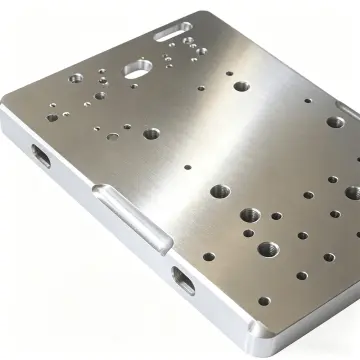
CNC Machining
3, 4, and 5-axis milling plus turn-mill centers for complex structural frames, sensor housings, and custom brackets. Critical tolerances held to ±0.005 mm.
 Explore CNC Machining Services →
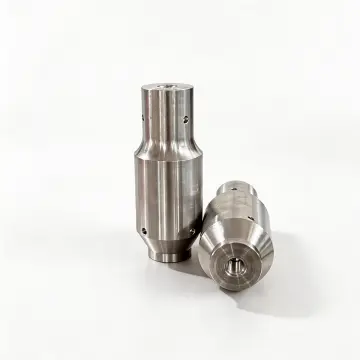
Precision Turned Parts
Swiss-type precision turning and multi-spindle lathes producing bushings, pins, retention plugs, ultrasonic boosters, and threaded fittings in brass, steel, and titanium.
 Explore Precision Turned Parts →
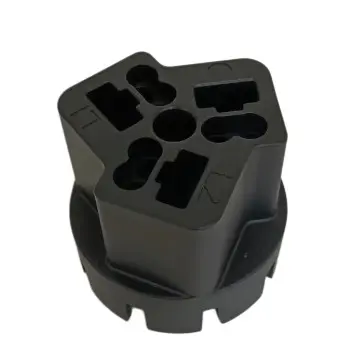
Plastic Injection Molding
Custom tooling fabrication, multi-cavity injection molding, insert molding, and overmolding. Complete Moldflow gate optimization and CMM inspection.
 Explore Molded Parts →
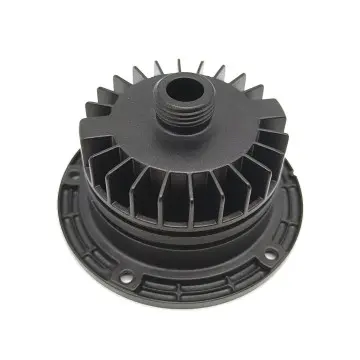
Die & Investment Casting
Aluminum and zinc high-pressure die casting, vacuum die casting, and investment casting for heat sinks, motor housings, pivot arms, and power enclosures.
 Explore Casting Capabilities →
Sheet Metal & Stamping
Progressive die stamping, laser profiling, CNC press brake bending, and busbar lamination. Producing motor stator/rotor laminations and terminal clips.
 Explore Stamping Capabilities →
Bridge Tooling & Prototyping
Bridge the gap between initial concept and mass tooling using industrial SLA/SLS 3D printing and vacuum urethane casting with silicone molds.
 Request Technical Process Catalog →
Global Compliance, Quality Documentation & IP Governance
Eliminate risk before your mold tooling is cut. Every project complies with international regulatory standards and verifiable documentation packages.
Full Inspection Dossiers
Every shipment is accompanied by detailed First Article Inspection (FAI) reports, full CMM coordinate measuring reports, and material spectrometer certifications establishing alloy and resin pedigree.
Rigid IP Protection Protocols
We execute legally binding bilateral Non-Disclosure Agreements (NDAs) prior to receiving 3D CAD geometry. Direct communication with our factory engineering team eliminates secondary broker exposure.
RoHS, REACH & Export Compliance
Raw materials and post-treatments (anodizing, electroplating, passivation) are strictly audited to RoHS and REACH restricted substances directives, guaranteeing frictionless customs clearance in the US, EU, and UK.
The Future of Precision Mold Fabrication & Smart Tooling
Advancing multi-cavity synchronization, closed-loop machine learning process adjustments, and sustainable circular polymers.
rPET & Bio-Based Polycondensates
Developing specialized hot runner nozzles with anti-corrosive PVD coatings designed to handle 100% post-consumer recycled PET (rPET) without flow streak defects or variable thermal degradation.
IoT-Enabled In-Cavity Pressure Telemetry
Integrating piezo-electric pressure and fiber-optic temperature sensors directly inside mold cavities, allowing live cavity pressure feedback to dynamically tune injection packing profiles in real time.
Additive Conformal Cooling Channels
Employing direct metal laser sintering (DMLS) 3D printing for hybrid mold core inserts, creating sub-surface spiral cooling passages that slash cycle times by 35% on thick-wall preforms.
Frequently Asked Questions for Sourcing & Tooling Engineers
In-depth responses regarding manufacturing capabilities, tooling lifespans, lead times, and export logistics.
What tolerances can Sunmy Hardware hold on custom tooling & CNC parts?
On critical CNC milled and turned features, our shop standard achieves ±0.005 mm (5 microns), while high-precision molding core and cavity components are routinely held to ±0.005 mm using high-speed optical jig grinding and wire EDM. Achievable tolerance is confirmed during the formal DFM stage.
How does Sunmy control moisture degradation during PET molding?
We deploy closed-loop desiccant honeycomb dryers with dew points maintained strictly below -40°C. Virgin and technical PET resins are dried for 4 to 6 hours at 160°C to guarantee moisture content stays below 0.005% (50 ppm), completely preventing hydrolytic IV degradation and brittle part failures.
Which operations are managed in-house versus partner networks?
CNC machining, precision Swiss turning, and metal stamping are carried out inside Sunmy-owned Shenzhen facilities. Large-scale die casting and specialized surface treatments run in audited partner plants. All First Article Inspections (FAI), CMM verification, and packaging QC are 100% handled in-house.
What is the typical lead time for injection mold tooling and FAI samples?
Rapid prototype tooling and bridge molds are completed in 10 to 18 business days. High-cavitation production tooling (e.g., 16 to 72 cavity hot-runner systems) typically takes 28 to 38 calendar days, including full mold flow verification, trial shots (T1), and comprehensive dimensional inspection reports.
How are international engineering drawings and NDAs handled?
We execute standard mutual NDAs directly via email before receiving native CAD files (STEP, IGES, X_T, DWG). Communication is held directly with bilingual mechanical engineers who provide a structured DFM feedback package within 24 hours.
Can you provide custom surface textures and optical SPI finishes?
Yes. Our mold polishing department provides up to SPI A-1 diamond mirror polish for optical lens barrels and clear preforms. For exterior enclosures, we execute Mold-Tech chemical etching, EDM spark textures, and bead-blasted matte finishes according to your CMF requirements.
Precision Robotic, Sensor & Industrial Assemblies
Engineered components manufactured from stainless steel, billet aluminum, and medical titanium alloys ready for worldwide air/sea deployment.








Request an Engineering DFM Review & Official Tooling Quote
Connect with Shenzhen Sunmy Hardware engineers directly. Share your 2D drawings with critical GD&T or 3D CAD files (.STEP, .IGES, .X_T) for comprehensive analysis, mold flow evaluation, and competitive volume pricing within 24 hours.