
High-Tolerance Precision Fabrications & Assemblies
Each component exemplifies our rigorous Design for Manufacturability (DFM) methodology, achieving structural integrity across brass, copper, aerospace-grade aluminum, and stainless steel.

High-Quality Precision Knurled Brass Threaded Connector
View Specs
ODM High-Performance Copper Heatsink Manufacturer
View Specs
ODM Custom CNC Machined Aluminum Vacuum Manifold Block
View Specs
Custom CNC Milled Aluminum Alloy Right Angle Mounting Bracket
View Specs
Custom CNC Machined Robot Finger Joint Link
View Specs
Custom CNC Turn-Milled Bayonet Mount & Locking Ring
View Specs
High-Quality Custom Precision Turned Stainless Steel Valve
View Specs
OEM Custom CNC Turned Hose Barb Fittings & Adapters
View SpecsPrecision Sheet Metal Engineering: Deterministic Quality & Structural Integration
Modern industrial manufacturing requires sheet metal fabrication to transition from coarse enclosure building to precision-engineered mechatronic assemblies. At Shenzhen Sunmy Hardware, we integrate state-of-the-art 12kW fiber laser cutting, multi-axis automated CNC press brakes, progressive-die stamping, and 5-axis CNC mill-turn centers under an audited single-source operational umbrella.
Micro-Tolerances & Bend Compensation
Sheet metal deformations are non-linear. By pre-calculating exact K-factors, material yield tensile limits, and grain orientation dynamics during CAD unbending, we preserve critical feature positions to ±0.05 mm across multi-stage press brake sequences.
Laser-Punch Hybrid Kinematics
Our automated TRUMPF-class punch-laser systems eliminate heat-affected zone (HAZ) stress on micro-perforations while generating precise countersinks, extruded taps, and louver geometry in a single, high-speed automated cycle.
Welding Integrity & Surface Aesthetics
From robotic CMT (Cold Metal Transfer) to automated handheld laser welding, we eliminate post-weld spatter, controlling distortion in thin-gauge enclosures. Finished surfaces meet Class-A cosmetic criteria under specular illumination.
China Factory Ecosystem: Unrivaled Velocity, Capital Efficiency & Tooling Agility
Why leading Fortune 500 OEMs consolidate their custom sheet metal and hybrid machining programs in Shenzhen: the convergence of raw material agility, hyper-dense precision tooling ecosystems, and direct tier-1 engineering accountability.
Shenzhen Ecosystem
Direct proximity to the world's most dense supply cluster of cold-rolled steel, copper alloys, AL6061-T6, and precision electroplating facilities within a 30km radius.
Rapid Prototype to Mass Run
Tooling and progressive die design fabricated in-house. First Article Inspection (FAI) reports turned around in under 72 hours with zero bureaucratic bottlenecks.
Total Cost of Ownership
Achieve 30% to 50% tooling and unit cost advantages compared to Western European or North American domestic shops, without sacrificing dimensional fidelity.
Direct Factory IP Protection
Eliminate unauthorized middleman broker networks. Strict NDAs are executed before CAD receipt, ensuring complete hardware architecture containment.
Precision Factory Operations & Real-Time Quality Control
Since 2016, Shenzhen Sunmy Hardware Co., Ltd. has delivered production-grade mechanical hardware to European and North American tier-1 markets with auditable CMM verification.
Micro-turned features and milled datums verified with multi-sensor ZEISS coordinate measuring machines.
High-speed mechanical and pneumatic stamping lines running continuous progressive-die configurations.
Comprehensive manufacturability audits on bend interference, tooling access, and tolerance stack-ups.
Full optical dimension reports, spectrometry alloy verification, and RoHS salt-spray compliance tracking.
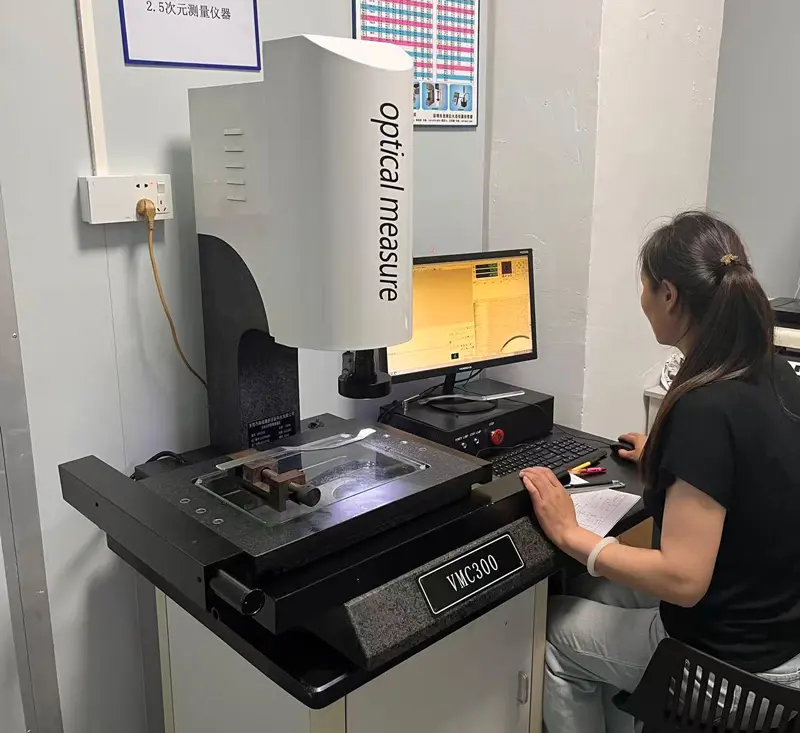
Precision Sheet Metal & CNC Machining Parameter Guidelines
Selecting optimal manufacturing protocols requires balancing mechanical tensile requirements, dimensional tolerancing, volume scaling, and per-unit economic thresholds.
| Manufacturing Process | Material Capabilities | Linear / Forming Tolerance | Surface Roughness (Ra) | Optimal Production Run | Target Applications |
|---|---|---|---|---|---|
| Fiber Laser Cutting (12kW) | Stainless Steel, AL5052/6061, Brass, Mild Steel (0.5mm – 25mm) | ±0.03 mm | Ra 1.6 – 3.2 µm | 1 – 50,000 units | High-precision blanks, complex apertures, optical breadboards |
| CNC Servo Press Brake | SPCC, SECC, Aluminum Sheets, Copper busbar alloy | ±0.05 mm / 0.2° | N/A (Tooling mark controlled) | 10 – 100,000 units | 19-inch rackmount chassis, mounting brackets, RF shield cans |
| Progressive Die Stamping | Cold-rolled steel, phosphor bronze, beryllium copper, silicon steel | ±0.01 mm | Ra 0.8 – 1.6 µm | 50,000 – 1,000,000+ | Motor laminations, spring clips, continuous battery terminals |
| 5-Axis CNC Machining | AL7075, Titanium Grade 5, Tool Steel, Engineering Plastics (PEEK, POM) | ±0.005 mm | Ra 0.4 – 0.8 µm | 1 – 10,000 units | Vacuum manifold blocks, drone universal joints, robotics knuckles |
| High-Speed Swiss Turning | Brass C3604, 316L Stainless, Copper C1100, Custom titanium | ±0.003 mm | Ra 0.2 – 0.4 µm | 500 – 500,000 units | Knurled pins, fluid connectors, bayonet locking rings, inserts |
Mission-Critical Applications in Global Industry Sectors
Sunmy Hardware sheet metal assemblies and micro-turned components are deployed across extreme environmental conditions worldwide, fulfilling the stringent mandates of international engineering bodies.
Telecom & High-Density Datacenters
EMI/RFI shielded 19" rack-mount chassis, cold-rolled perforated ventilation panels with 70%+ open area ratio for optimized thermal aerodynamics, and tight-tolerance slide rail brackets.
EV Powertrain & Energy Storage
Laminated and nickel-plated flexible copper busbars, lightweight aluminum battery pack shells, vibration-damped structural trays, and cold plates engineered for continuous thermal dissipation.
Medical Equipment & Lab Analytics
Stainless steel 316L fluid manifolds, hermetically welded optical breadboards, anti-microbial powder coated outer shells, and high-precision sensor brackets with absolute zero burr tolerances.
Industrial Robotics & Automated Gantries
Structural joint links, 6-axis torque sensor housings, cable carrier assemblies, and deep-drawn motor protection covers tested to withstand millions of continuous vibration cycles.
Aerospace & Autonomous Drones
Ultra-thin 5-axis milled titanium gearbox housings, aluminum AL7075-T6 airframe mounting plates, and high-reliability locking ring interfaces with weight-minimized pockets.
Solar Inverters & Outdoor Smart Grid
Weather-resistant marine-grade powder-coated enclosures, extruded aluminum heat sink cases with integrated sealing gasket channels, and laser-cut busbar connections.
Real Engineering Case Studies: Root-Cause Remediation & Scaled Delivery
Global hardware brands frequently engage Sunmy Hardware after previous domestic or overseas suppliers fail due to cumulative tolerance stack-ups or metallurgical porosity.
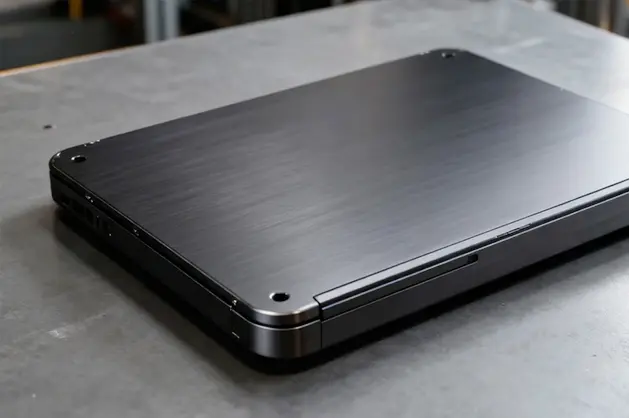
Aluminum Alloy Chassis Tolerancing
Challenge: An incumbent supplier suffered from 0.12mm warping after sandblasting and anodization, preventing clean snapped closure in high-volume assembly lines.
Engineering Solution: Sunmy re-engineered tool cutter engagement paths, incorporated stress-relief annealing before final skim passes, and introduced optical CMM coordinate verification.
Result: Positional accuracy increased to 0.03mm; assembly cycle time was reduced by 40% across 250,000 units.
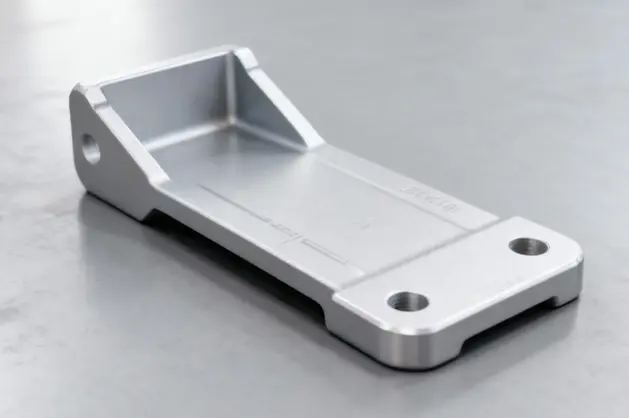
High-Stress Structural Mounting Bracket
Challenge: Micro-porosity within gravity die-cast brackets caused stress fractures during dynamic vehicle shock loading tests.
Engineering Solution: Switched to high-pressure vacuum die casting with optimized runner gate placement, finished via precision 5-axis CNC datum cuts, and protected with automotive electro-coating.
Result: 80% reduction in gas porosity, total elimination of deformation, passing 960 hours of neutral salt spray.
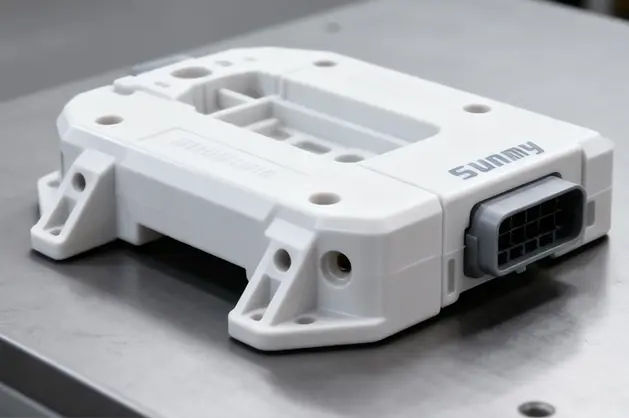
Integrated Mechatronic Gear Enclosure
Challenge: Severe sink marks and weld lines in high-glass-fill engineering polymers resulted in gear train misalignment under sustained mechanical torque.
Engineering Solution: Applied Moldflow volumetric shrinkage algorithms, relocated submerged injection gates, regulated mold heating channels, and tightened parting line seal tolerances.
Result: Zero sink mark defects, 25% increase in load capacity, securing continuous multi-year OEM volume awards.
Macro Sourcing Trends: The Future of Precision Sheet Metal & CNC
Navigating trade evolutions, automated bending kinematics, closed-loop optical quality inspections, and sustainable industrial carbon compliance.
Smart Industry 4.0 Sheet Metal
Integration of real-time laser thickness sensors and automated robotic press brake arms capable of dynamically adjusting bending force based on batch-specific metallurgical springback measurements.
Single-Setup Hybrid Machining
Eliminating multi-fixture accumulated error by pairing high-speed sheet metal forming directly with 5-axis mill-turn centers for precision threaded bosses, o-ring grooves, and optical datum locations.
Green & Circular Manufacturing
EU CBAM (Carbon Border Adjustment Mechanism) readiness, near-100% recycling of ferrous and non-ferrous swarf, zero-discharge wastewater anodizing, and non-toxic RoHS/REACH passivation chemistry.
5-Stage Zero-Defect Manufacturing Pipeline
How we transform your raw 3D CAD/STEP packages into calibrated, serial-tracked hardware shipped straight to your overseas assembly facility.
CAD/DFM Submission
Initial design upload (.STEP, .IGES, 2D PDF with GD&T). Our engineers perform tolerance stack-up and bend interference audits within 24 hours.
Mutual NDA & Quoting
Direct non-disclosure agreement protection. Transparent tooling amortization and piece-part cost breakdowns with guaranteed raw material lock-in.
First Article (FAI)
Rapid CNC/laser prototyping. In-house CMM dimensional validation, material chemical analysis, and First Article documentation approved by your engineering team.
Volume Production
Automated press brake and stamping run. SPC (Statistical Process Control) checks at critical workstations to maintain 100% CPK repeatability.
Global Export & Customs
Custom protective blister or vacuum packaging, humidity indicators, export crating, and direct DDP/CIF logistics to ports worldwide.
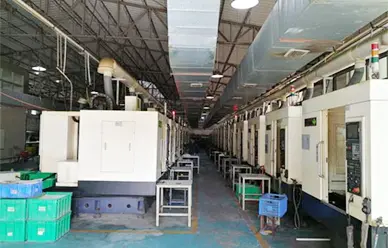
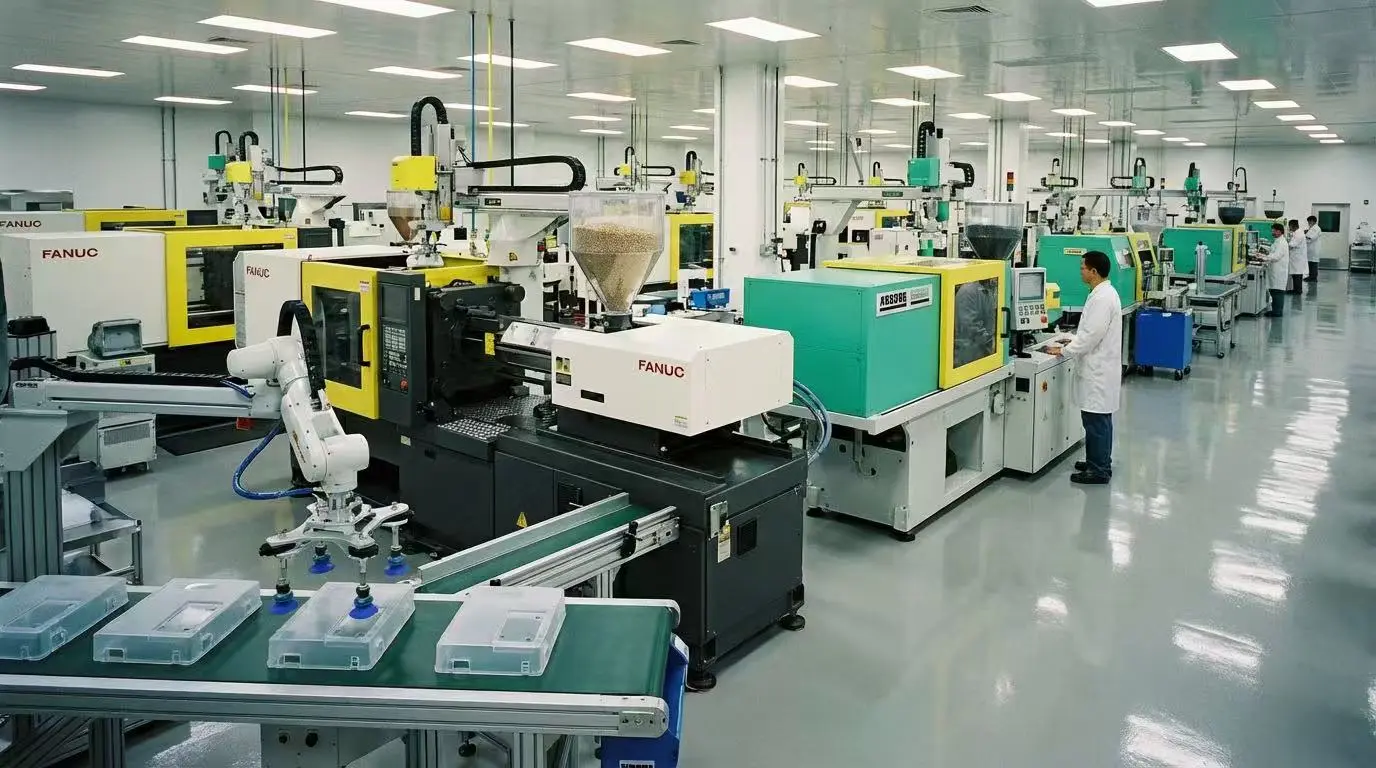
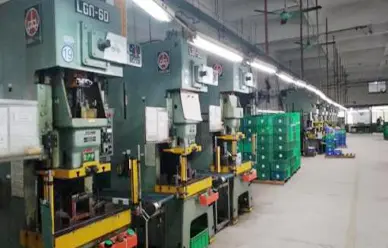
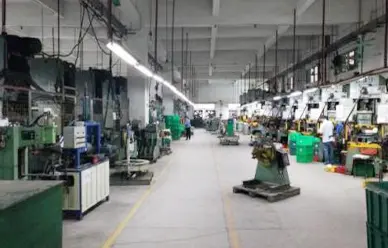
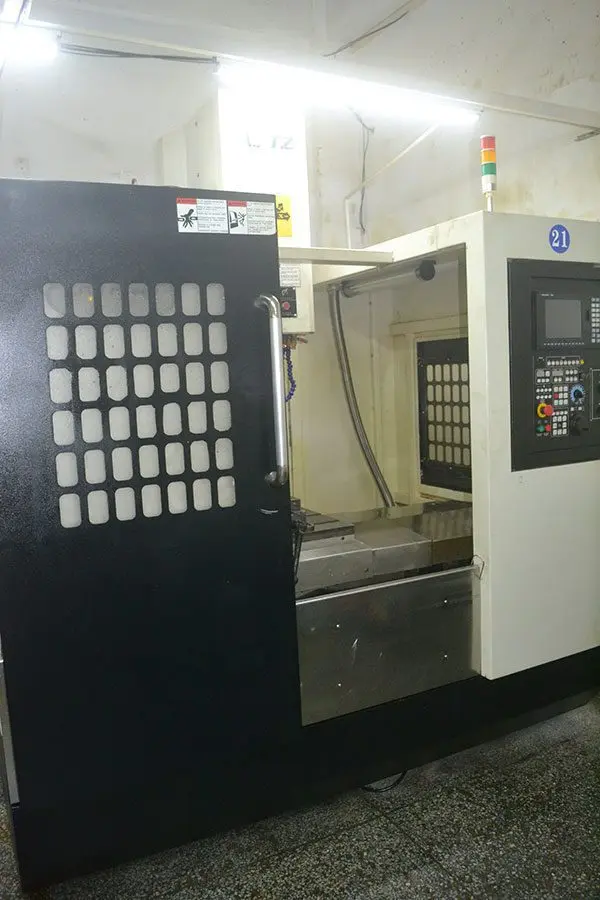
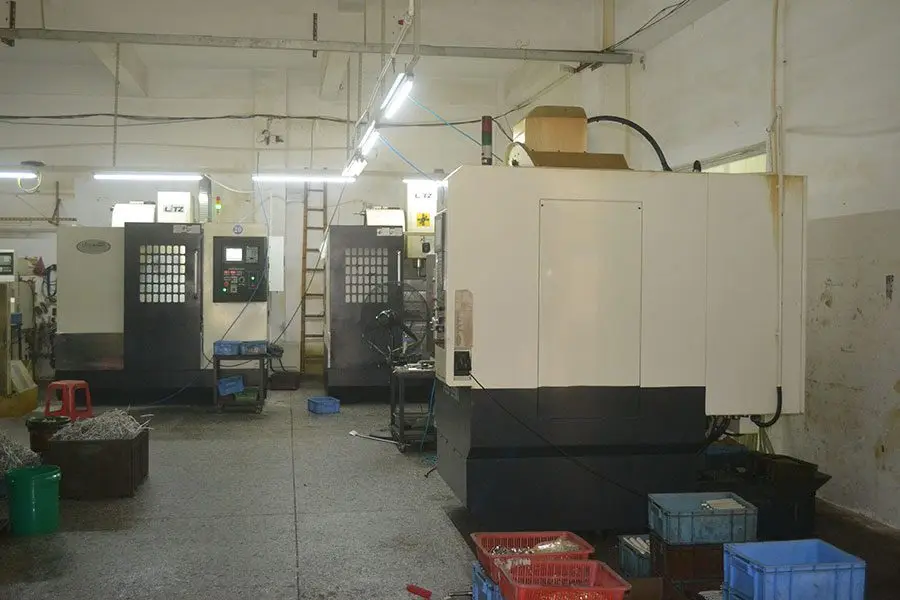
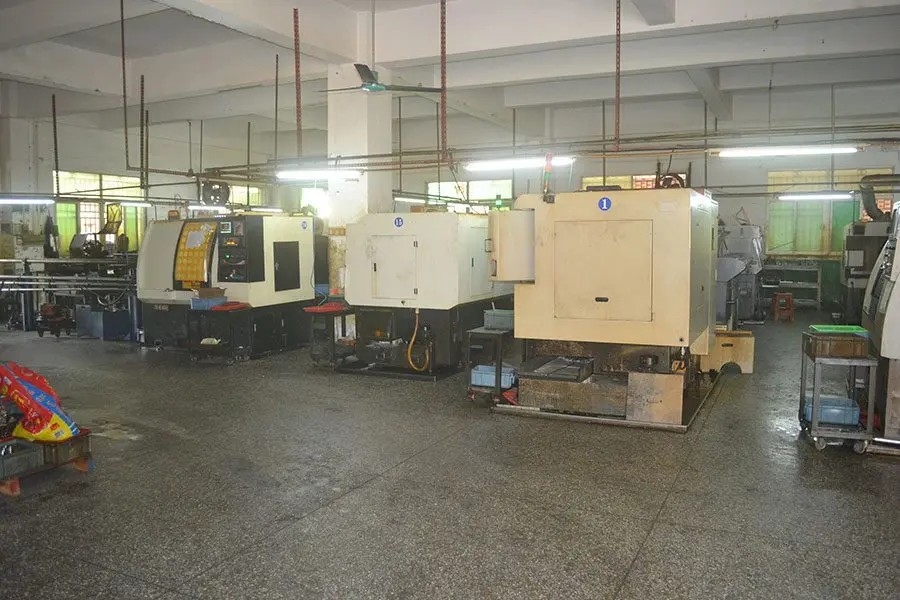
Inside the Sunmy Manufacturing Workshops
Modern plant floors in Shenzhen equipped with high-speed automated machinery, multi-axis machining cells, and dedicated CMM metrology labs.
Auditable Quality Systems: ISO, RoHS & Traceable Metallurgical Integrity
Quality claims require absolute physical proof. Sunmy maintains strict adherence to standardized quality management frameworks, with verified inspection records accompanying every batch.
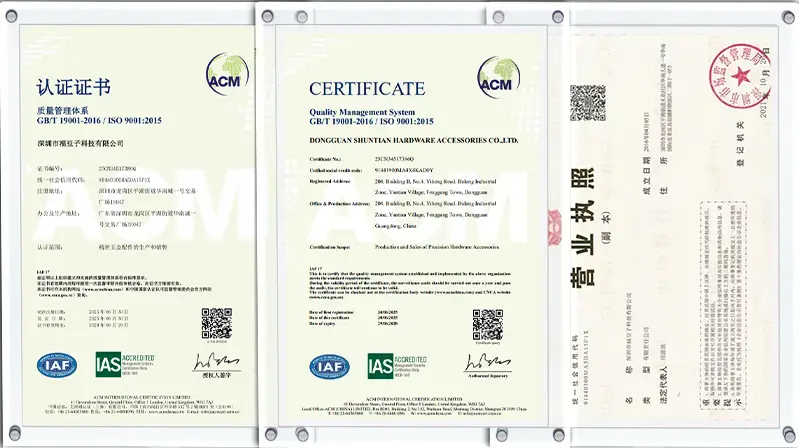
ISO Certified Quality Management
Strictly maintained incoming material verification (IQC), in-process statistical process control (IPQC), and final outgoing inspection (OQC).
Full Material Certifications (MTRs)
Mill test certificates, spectrometry chemical breakdowns, and tensile stress test records delivered with all non-ferrous and steel batches.
RoHS & REACH Chemical Compliance
Heavy metal ban conformity for lead, cadmium, mercury, and hexavalent chromium, qualifying parts for immediate European market integration.
Frequently Asked Questions: Sheet Metal & Custom CNC Sourcing
Clear, direct answers addressing engineering tolerances, IP security, rapid prototypes, tooling lifespans, and logistics management.
What tolerances can Sunmy Hardware maintain on precision sheet metal parts?
How does Sunmy guarantee IP protection when handling confidential CAD drawings?
Which manufacturing processes are run in-house versus through certified partners?
Can you assist in Design for Manufacturability (DFM) to reduce sheet metal costs?
What surface finishing services are available for custom metal enclosures?
What is your typical lead time for prototypes versus volume production runs?
How do you manage international shipping, customs, and export packaging?
What documentation is provided with each shipped hardware consignment?
Precision Turned, Machined & Stamped Hardware Solutions
Browse additional mission-critical hardware engineered and verified at our Shenzhen manufacturing facility.

Custom Self-Tapping Threaded Inserts Product
View Specs
Precision CNC Solid Aluminum Optical Breadboard
View Specs
Flexible Laminated Copper Busbar for Battery & Electrical
View Specs
High-Quality Custom Wedge-Lock Washer Pairs Product
View Specs
ODM Custom CNC Precision Turned Stainless Filter Sleeve
View Specs
Precision CNC Machined High-Voltage Insulator Contact Base
View Specs
5-Axis CNC Machined Joint Base & Gearbox Shell
View Specs
CNC Machined Aluminum Enclosure for RF Sensor Modules
View SpecsAccelerate Your Custom Metal Fabrication Project
Send your 2D drawings (.PDF, .DWG) and 3D models (.STEP, .STP, .X_T) for rapid DFM evaluation. Receive comprehensive tolerancing feedback and binding quotations within 24 hours.