
Featured Custom CNC & Precision Components
Directly from our Shenzhen production lines. Every batch is manufactured from certified billets and verified on Zeiss/Mitutoyo CMMs.

High-Quality Custom CNC Machining Brass Insert Connector with Knurled Pin
View Specifications


ODM Custom Precision Turned Stainless Steel Filter Sleeve (Industrial Grade)
View Specifications

ODM OEM Precision CNC Machining Aluminum Parts & Custom Industrial Components
View Specifications
OEM Custom Precision CNC Machined Aluminum Hinge Assembly Connector
View Specifications
High-Precision CNC Machined Metal Bracket & Frame Wire EDM Milling
View SpecificationsAluminum Alloy Metallurgy & Machinability Dynamics
Selecting the optimal alloy substrate dictates chip formation, thermal distortion mitigation, toolpath harmonics, and final surface integrity in precision CNC milling.
Technical Principle: Controlling Residual Stress in Thin-Walled Structures
High-speed aluminum machining frequently induces internal tensile-compressive stress rebalancing, leading to dimensional warping post-unclamping. Sunmy Hardware deploys specialized pre-stretched wrought tooling plates (e.g., Alimex, MIC-6, and aerospace-certified 6061-T651 / 7075-T7351) paired with multi-stage roughing-finishing cycles, cryogenic stress relief, and high-frequency dynamic chip breaking to ensure geometric flatness within 0.02 mm across spans greater than 500 mm.
| Alloy Grade | Composition Characteristics | Tensile Strength (MPa) | Machinability Index | Typical Critical Application |
|---|---|---|---|---|
| 6061-T6 / T651 | Mg-Si alloy; high toughness, superior corrosion resistance, excellent TIG/MIG weldability. | 290 – 310 | High (Clean continuous chips) | Robotics chassis, optical brackets, structural plates, automation frames. |
| 7075-T651 | Zn-Mg-Cu alloy; extreme strength-to-weight ratio, comparable to structural steel. | 540 – 570 | Moderate (Requires carbide CVD/DLC tools) | Aerospace structural ribs, rocketry gimbals, high-stress defense connectors. |
| 2024-T3 / T351 | Cu-Mg alloy; exceptional cyclic fatigue resistance, high fracture toughness. | 440 – 480 | High (Susceptible to atmospheric corrosion) | Aircraft fuselage tension members, avionics instrument gear housings. |
| 5083-H111 | Non-heat-treatable Mg alloy; ultimate resistance to sea water and harsh cryogenic chemical attacks. | 275 – 350 | Fair (Tends to gummy chip formation) | Subsea sensor housings, marine instrumentation, cryo-pressure flanges. |
| MIC-6 ® Tooling | Continuous-cast modified aluminum plate; virtually zero internal residual stress. | 165 – 180 | Superior (Ultra-high surface finish Ra < 0.2) | Semiconductor vacuum chucks, wafer handling tables, laser optical benches. |
Metallurgical Anisotropy Control
Extruded versus rolled plate billets exhibit marked microstructural grain alignment variations. Sunmy verifies billet grain orientation relative to primary stress vectors, avoiding shear failure in thin-walled avionic assemblies.
Thermal Coefficient Compensation
With aluminum's high thermal expansion coefficient (~23 × 10⁻⁶/K), spindle-induced friction alters part dimensions in-cycle. Our constant-temperature workshops (20°C ± 1°C) eliminate thermal growth errors.
Material Certification EN 10204 3.1
Every shipment is backed by authenticated chemical spectrometry and mechanical tensile test reports directly linked to raw ingot heat numbers, ensuring total trace-level metallurgical transparency.
The Greater Bay Area Precision Ecosystem Advantage
Why global engineering leaders anchor custom CNC manufacturing programs in Shenzhen: compressed lead times, localized tier-1 supply networks, and unmatched technological scalability.
The 30-Kilometer Supply Radius
Within 30 minutes of our Shenzhen facility lies the world's densest concentration of certified anodizing lines, wire EDM centers, precision tooling specialists, and metallurgical test laboratories. Secondary processes that take 3 weeks in the West are executed in 48 hours.
Direct Factory Senior Engineering
Sunmy Hardware eliminates trading middleman friction. Global procurement teams converse directly with bilingual senior CAM/DFM engineers. Tooling pathways, fixturing strategies, and GD&T clarifications occur in real-time, saving up to 40% in pre-production iteration cycles.
Elastic Scale: Prototype to Mass Rollout
Seamlessly transition from single-unit NPI (New Product Introduction) engineering validation units to 500,000+ unit high-volume runs. We deploy modular tombstone fixturing on horizontal 4-axis centers and automated pallet changers to maintain ultra-low unit costs.
Multi-Process Bridge Technology
When CNC volumes exceed economical thresholds, our facility seamlessly converts parts into high-pressure aluminum die casting or progressive die stamping, maintaining all CMM inspection standards and surface anodizing specs under one roof.
Micron-Level Tolerancing, GD&T & CMM Inspection Protocols
Executing precision is an engineering science. How Sunmy Hardware translates ASME Y14.5 and ISO 2768-mK geometric requirements into physically validated components.
True Position ≤ 0.01 mm
Maintaining tight geometric relationships across complex multi-axis features. We utilize in-process Renishaw tactile probing systems for dynamic datum alignment, ensuring pitch centers and threaded inserts remain perfectly concentric across production batches.
Surface Topology Ra 0.4 – 0.8 μm
Surface finish directly determines seal vacuum integrity and fatigue resistance. Utilizing balanced high-speed spindles (up to 30,000 RPM) with mono-crystalline diamond tooling, we achieve mirror finishes and precise micro-groove fluid channels without hand-polishing distortions.
AS9102 First Article Inspection (FAI)
Prior to volume production release, our quality department executes full-dimension ballooned drawings and AS9102 Rev B FAI reports. Every linear, angular, and GD&T callout is cross-checked using coordinate measuring machines with calibrated laser scanning heads.
Navigating Global OEM Sourcing Pain Points
Addressing tariff landscapes, IP confidentiality, regulatory compliance, and cross-border freight predictability for European and North American engineering enterprises.
Rigorous IP Protection Infrastructure
Proprietary designs are shielded via formal bilateral NDAs. STEP/CAD models reside on isolated, encrypted internal servers. Physical plant access is restricted via biometric authorization, safeguarding patented geometry from competitive leaks.
RoHS, REACH & Conflict Mineral Compliance
EU and US markets demand rigorous environmental traceability. All our aluminum extruded profiles, hex bar stock, and surface passivations (such as SurTec 650 and trivalent chromium coatings) comply with EU RoHS 2011/65/EU and REACH regulations.
Incoterms 2020: Frictionless DDP Delivery
We eliminate customs clearance risks by offering door-to-door Delivered Duty Paid (DDP) logistics via air express (FedEx/DHL) or temperature-controlled sea freight directly to customer warehouses across the USA, Germany, Japan, and the UK.
Total Traceability & Batch Quarantine
Each production run is laser-etched with serialized matrix codes. From raw billet foundry melt heat numbers to the specific CNC machining center and cutting tool batch, any anomaly is immediately traceable to prevent downstream recall liability.
Localized Application Scenarios & Case Implementations
Where Sunmy Hardware's precision CNC aluminum components operate: from aerospace flight systems to cleanroom semiconductor equipment.
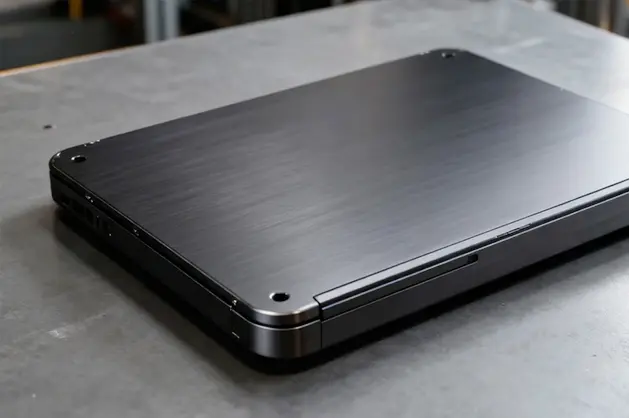
Precision Unibody Chassis
Monolithic unibody enclosure with complex interior pocketing, integrated heat pipe conduits, and bead-blasted Class A cosmetic finish with zero tooling witness marks.
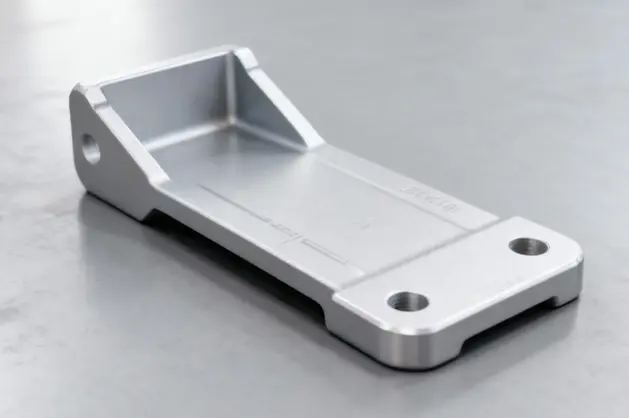
EV Inverter Support Bracket
Hybrid processing combining vacuum die-casting for lightweight web structures with CNC post-machining on high-load bearing mount points and O-ring sealing grooves.
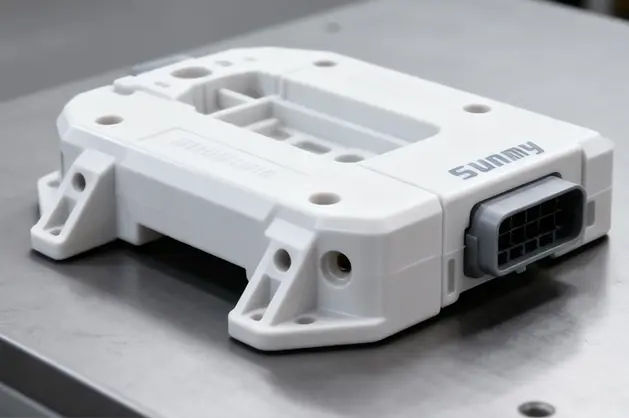
6-Axis Sensor Housing & Flexures
High-sensitivity mechanical elastic elements and robotic wrist end-of-arm tooling plates machined to tight coaxiality for precision load cell instrumentation.
Surface Treatment, Passivation & Coating Matrix
Precision aluminum machining requires carefully engineered chemical, electrochemical, and conversion finishes to satisfy electrical, thermal, and corrosion requirements.
Type III Hard Anodizing (MIL-A-8625)
Generates a dense oxide barrier layer (up to 50 μm) achieving surface hardness above 60 Rockwell C. Exceptional wear resistance for sliding components, hydraulic valve manifolds, and robotic gears.
Type II Decorative Color Anodizing
Precision color matching with controlled pore size absorption. Delivers vibrant, UV-stable cosmetic surfaces across deep black, gunmetal titanium, champagne gold, and customer-specified RAL shades.
Chemical Conversion (SurTec 650 / Alodine)
MIL-DTL-5541F compliant trivalent chromium passivation preserving electrical grounding conductivity while protecting aerospace chassis from galvanic oxidation in humid operating zones.
Electroless Nickel & Micro-Arc Oxidation
Uniform deposit thickness inside blind holes and deep recesses without edge build-up. Ideal for harsh chemical exposure, high dielectric resistance, and semiconductor cleanroom applications.
The Next Horizon in Precision CNC Machining
Industry shifts shaping 2026–2030 manufacturing: generative design integration, closed-loop machine tool metrology, and green circular aluminum sourcing.
AI-Accelerated CAM & Adaptive Feeds
Neural CAM algorithms simulate real-time cutting tool chatter and spindle deflection, dynamically modulating feed rates to prevent tool vibration. This reduces milling cycle times by 28% while extending micro-tool lifespan.
Low-Carbon & Closed-Loop Swarf Recovery
Aligning with European CBAM carbon border directives, Sunmy segregates clean 6000 and 7000 series aluminum swarf for 100% direct recycling back into certified billets, lowering the embodied carbon footprint by up to 65% per component.
In-Situ Closed-Loop Metrology
Machine tools equipped with optical contact probes measure critical datums directly in the fixture. If tool wear or thermal expansion causes deviation, the CNC controller automatically offsets tool geometry before the finishing pass is completed.
Built for Auditable Engineering Repeatability
Founded in 2016, our facility operates proprietary CNC milling, turn-mill, stamping, and quality validation labs serving global engineering teams.
Critical CNC Tolerance Verified via CMM
In-House FAI & Dimensional Quality Check
Annual Precision Stamping & Casting Output
DFM Engineering Review & Quotation Turnaround
Frequently Asked Questions for Engineering Buyers
Direct technical answers addressing machining tolerances, surface treatments, material certs, tariffs, and engineering collaboration.
What tolerances can Sunmy Hardware hold on custom CNC machined aluminum parts?
How do you prevent warping and distortion in thin-walled aluminum components?
What quality inspection documentation accompanies each export shipment?
How do you protect 3D CAD files and customer intellectual property (IP)?
Which manufacturing operations are performed in-house vs. outsourced?
Can Sunmy support low-volume prototyping and scale into mass manufacturing?
How fast can our engineering team expect a quote and DFM report?
How do you handle shipping, international customs, and DDP terms?
Specialized Precision Turned & Engineered Parts
Complementing our aluminum CNC expertise with stainless steel Swiss micro-turning, robotics end-effectors, copper busbars, and titanium ultrasonic systems.

High-Quality Custom Precision Capillary Stainless Steel Pipe / Tube (OD 1mm - 8mm)
View Specifications
China Custom CNC Machined Foam Vacuum Gripper Plates for Robotic EOAT
View Specifications
Custom CNC Turn-Milled Bayonet Mount & Locking Ring Optical Component
View Specifications
OEM Custom CNC Turned Hose Barb Fittings & Threaded Hydraulic Adapters
View Specifications
ODM Custom Hollow-Shaft Cycloidal Reducer OEM Parts & Sub-Assembly
View Specifications
OEM Custom Stainless Steel Waterproof Sensor Probe Housing & Thermowell
View Specifications
Custom Flexible Laminated Copper Busbar for Battery & Electrical Equipment
View Specifications
ODM Custom Titanium Ultrasonic Booster Resonance Precision Turned Horn
View SpecificationsReady to Transition Your CAD into Production?
Send your engineering drawings and GD&T specifications directly to our Shenzhen technical office. An experienced CAM/DFM project engineer will analyze your requirements and respond within 24 hours.