
Engineered CNC Components: Top High-Precision Systems
Verified sub-tier supply chain assemblies manufactured via 3, 4, and 5-axis CNC setups with integrated Coordinate Measuring Machine (CMM) reports.








Navigating Global OEM Sourcing Paradigms
In an era characterized by dynamic global supply chains, international engineering buyers across North America, Europe, and Asia-Pacific require more than transactional manufacturing. Sourcing directors demand strategic tier-1 partners capable of mitigating volatility, securing technical IP, and guaranteeing repeatable metallurgical and geometric precision.
Intellectual Property & Direct Channel
Engineering drawings sent to broker houses risk uncontrolled distribution. Sunmy Hardware operates a strict factory-direct model: bilateral NDAs prior to STEP/CAD ingesting, proprietary data vaulting, and zero third-party brokering, assuring full legal protection.
Total Cost of Ownership (TCO)
Cheap unit rates frequently conceal secondary scrap rates, late assembly lines, and high rework costs. Our in-house DFM analysis optimizes cycle times, tool paths, and raw billet sizing to deliver lower landed TCO without compromising geometric fidelity.
High-Mix Low-Volume to Mass Scaling
Eliminate supplier re-qualification friction. Leverage rapid CNC prototyping and bridge tooling, scaling smoothly into automated horizontal CNC machining centers, high-pressure die casting, and progressive stamping dies under a singular engineering team.
Macro-Industry Engineering Solutions
Tailored manufacturing workflows certified to address sector-specific thermal, mechanical, chemical, and strict compliance boundaries.
Aerospace & Defense
Precision 5-axis milling of 7075-T6 aluminum, titanium Grade 5, and Inconel. Structural weight optimization via thin-wall CNC pockets, vibration damping brackets, and MIL-spec surface treatments including chemical conversion and hard anodizing.
Medical & Surgical Devices
Swiss lathe turned titanium micro-screws, orthodontic anchors, 316L surgical retractors, and biocompatible endoscopic valve components. Micro-burr control under 40x magnification, passivation, and ultrasonic cleanroom packaging.
Semicon & Optical Optics
8-inch aluminum wafer carriers, chamber vacuum manifolds, and optical lens barrels. Strict flatness (<0.01 mm) and coaxiality controls with low-outgassing finishes preventing molecular contamination inside wafer fab systems.
Robotics & Drone Systems
Multi-axis robotic gripper jaws, lightweight universal joint bases, gearbox housings, and 6-axis force/torque sensor elastic flexures machined to sub-micron accuracy for ultra-responsive dynamic motion feedback.
Engineering Capability & Tolerance Matrix
Standard, advanced, and critical process thresholds across Sunmy Hardware’s manufacturing footprint.
| Manufacturing Technology | Supported Materials | Achievable Tolerance | Standard Surface Roughness | Typical Applications |
|---|---|---|---|---|
| 5-Axis CNC Milling | AL6061-T6, 7075-T6, SUS304/316, Titanium Gr5, PEEK | ±0.005 mm (±0.0002 in) | Ra 0.4 – 0.8 μm | Complex aerospace brackets, robotic housings, sensor bases |
| Swiss Precision Turning | Stainless steel, Brass (C3604), Titanium, POM, Nitronic | ±0.003 mm (±0.0001 in) | Ra 0.2 – 0.4 μm | Orthodontic pins, medical needle sleeves, stepped shafts |
| Vacuum Die Casting + CNC | ADC12, A380, Zamak 3, Zamak 5 | ±0.025 mm (post-machined) | Ra 1.6 – 3.2 μm | High-volume automotive housings, electronic chassis |
| Progressive Stamping | SPCC, Copper, Beryllium Copper, Silicon Steel | ±0.015 mm | Process dependent | Motor laminations, spring clips, grounding terminals |
| Precision Injection Molding | ABS, PC, Nylon (PA66+GF), PEEK, TPU | ±0.020 mm | SPI-A2 (Diamond finish) | Enclosure shells, internal functional gears, cable link tracks |
Engineering Case Records: Root Cause to Production
Verifiable field data demonstrating how Sunmy Hardware resolves complex dimensional and mechanical bottlenecks.
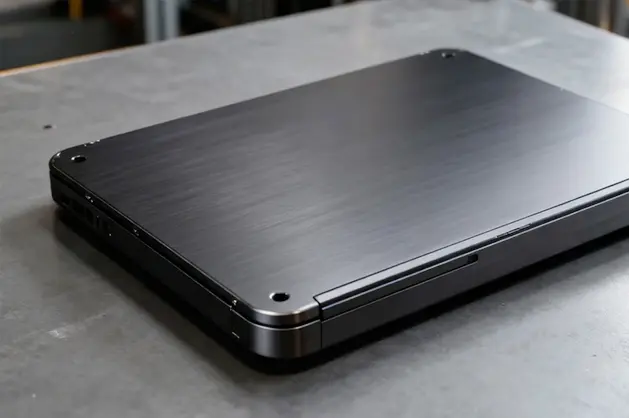
Case CS-01: Aluminum Alloy Enclosure
Sector: Consumer Electronics | Process: CNC + Sandblast + Anodizing
Challenge: Preceding tier-2 vendor could not maintain flatness and mating dimensions, yielding 2.8mm fitment gaps and erratic lines.
Resolution: Engineered specialized vacuum chucks, calibrated toolpaths, tightened critical tolerances, and applied 100% CMM verification.
Result: +0.03 mm dimensional gain, +40% assembly line efficiency, and entire series contracted to Sunmy.
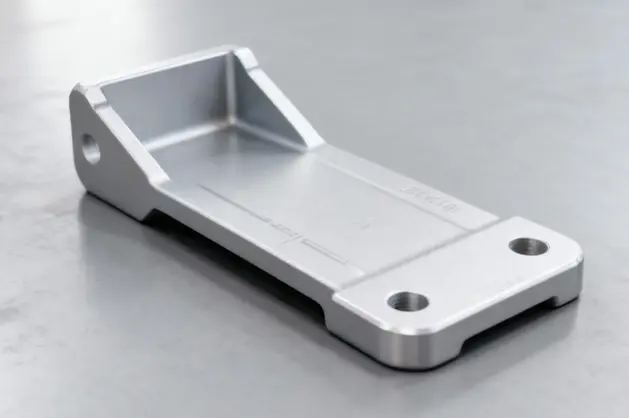
Case CS-02: Die-Cast Aluminum Bracket
Sector: Automotive OEM | Process: Die Cast + CNC Post + Powder Coat
Challenge: Micro-porosity pockets and warping caused salt-spray blistering and structural fatigue under cyclic stress.
Resolution: Re-engineered runner/gate geometry, deployed vacuum-assisted cold-chamber die casting, and built dedicated CNC milling fixtures.
Result: -80% porosity defect reduction, deformation clamped within ≤0.15 mm, 1000h salt spray pass, OEM tier-1 entry.
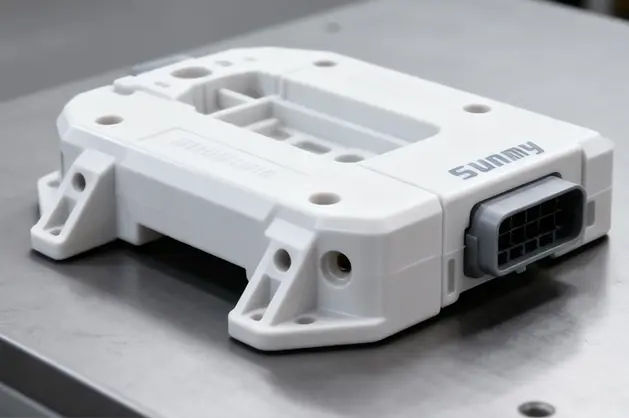
Case CS-03: Robot Functional Modules
Sector: Industrial Robotics | Process: Injection Molding + Silk Screen
Challenge: Sink marks around internal rib sections and short shots weakened load-bearing finger joints under cyclic tension.
Resolution: Conducted comprehensive Moldflow thermal analysis, rebalanced gating, optimized cooling channels, and fine-tuned packing profiles.
Result: Zero sink mark defects, +25% mechanical tensile capacity, and 7 follow-on robotics programs awarded.
Technology Roadmap: Intelligent Precision Machining
Pioneering Industry 4.0 data models, automated sub-micron compensation, and green closed-loop metallurgy for next-generation hardware.
In-Situ Closed-Loop Probing
Renishaw optical touch probes installed across all 5-axis work centers for automated datum setup, dynamic thermal-drift compensation, and in-machine feature verification before unchucking.
Automated Lights-Out Palletization
Robotic pallet changers servicing multi-axis milling cells, facilitating continuous 24/7 unassisted batch manufacturing with real-time tool breakage and wear monitoring sensors.
AI Tool Wear & Chatter Suppression
Edge-AI acoustic and harmonic spindle vibration analysis to proactively suppress harmonic chatter, maximizing cutting speeds and achieving mirror surface finishes down to Ra 0.1 μm.
Carbon Footprint & Metal Traceability
100% chip briquetting and certified alloy recycling loops. Direct carbon accounting per part to meet EU CBAM and corporate ESG sourcing directives without pricing premiums.
Quality Infrastructure, Traceability & Global Compliance
Every production lot is governed by standardized aerospace-grade metrology protocols and international regulatory compliance.
CMM Metrology & FAI Deliverables
Our climate-controlled inspection lab features high-precision bridge Coordinate Measuring Machines (CMM), optical video measuring systems (VMS), and surface profilometers. AS9102-compliant First Article Inspection (FAI) reports accompany all pre-production samples.
Metallurgical Traceability (EN 10204 3.1)
We eliminate counterfeit or substandard alloy risks. All incoming raw billets undergo optical emission spectrometer (OES) chemical verification. We furnish EN 10204 Type 3.1 material certificates with full heat/lot traceability back to the primary mill.
Logistics, Incoterms & Compliance
Full compliance with RoHS, REACH, and California Prop 65. Our logistics export division provides turnkey DDP, DAP, and CIF logistics options via air, express, or ocean freight with direct electronic customs clearance documents to EU, US, and UK ports.
Frequently Asked Sourcing & Technical Questions
Detailed operational insights addressing common qualification inquiries submitted by global procurement managers.
Featured Industrial Components: Turnkey Series
Robotics, fluid regulation, wafer handling, and biomedical parts engineered to precise client CAD boundaries.







Accelerate Your Manufacturing Program Today
Upload your 3D models and 2D engineering packages. Receive a comprehensive DFM technical analysis and cost evaluation directly from our senior machining staff within 24 hours.