

Precision Engineering Catalog
High-Performance Custom CNC Motorcycle & Robotic Components
Explore our export-certified CNC machining and precision-turned hardware portfolio. Each component is manufactured from aerospace-grade alloys, subjected to multi-axis tolerance verification, and backed by complete material traceability.







Industry Technical Whitepaper
Engineering Precision: Custom CNC Motorcycle Parts Manufacturing
High-performance powersports and custom motorcycle manufacturing represent one of the most mechanically demanding segments of modern precision machining. Unlike static industrial enclosures, motorcycle components operate continuously under dynamic cyclic vibration, torsional shear loads, extreme thermal gradients, and direct corrosive exposure.
Uncompromising Structural Integrity
Motorcycle chassis, suspension yokes, and brake caliper mounts demand structural predictability. We utilize stress-relieved forged billets (such as 6061-T6 and 7075-T651) that eliminate porosity, micro-fissures, and anisotropic grain boundaries inherent in traditional gravity die castings, ensuring ultimate tensile yield strength under track conditions.
5-Axis Simultaneous Kinematics
Modern aerodynamic fairing mounts, variable-rake triple clamps, and hollow-spoke wheel hubs demand complex continuous tool vectors. Our German and Japanese 5-axis machining centers eliminate stacked positioning errors by executing 3D contoured surfaces, deep pocket undercut drafts, and multi-axis bore alignments in a single clamping setup.
Extreme Environmental Durability
Exposed components face UV radiation, road de-icing salts, gravel impingement, and thermal cycling from 120°C engine blocks. We integrate Mil-Spec Type III Hardcoat Anodizing (MIL-A-8625), PVD titanium carbonitride coatings, and passivation protocols to safeguard metallurgical integrity and prevent galvanic corrosion.
International Certification & Risk Mitigation
Localized Technical Support & Global Regulatory Compliance
Exporting high-precision custom motorcycle components into North American, European, and Japanese tier-one markets necessitates rigorous adherence to vehicular safety mandates. Sunmy Hardware bridges Chinese factory-direct pricing with stringent Western compliance engineering.
TÜV Rheinland & ABE Homologation
Safety-critical structural components—including triple tree clamps, clip-on handlebars, rearsets, and brake levers—must comply with German Road Traffic Licensing Regulations (StVZO). We provide structural FEA simulations, destructive yield documentation, and chemical composition certs necessary for Allgemeine Betriebserlaubnis (ABE) certification.
DOT / FMVSS Compliance
For custom wheel hubs, hydraulic reservoirs, caliper adaptors, and lighting housings exported to the US market, our engineering department ensures design geometry conforms to Federal Motor Vehicle Safety Standards (FMVSS 106 for hydraulic brake assemblies and FMVSS 122 for motorcycle braking systems).
RoHS & REACH Metallurgical Audits
Every shipment destined for the European Union is backed by third-party spectroscopic inspection verifying zero restricted hexavalent chromium in passivation baths, total lead compliance in free-machining brass alloys (<0.1% Pb under EU RoHS exemptions), and zero PFAS contaminants in degreasing solvents.
EN 10204 3.1 Traceability
We eliminate metallurgical uncertainty. Every production run originates from certified billet stock with verified heat numbers. Clients receive EN 10204 Type 3.1 Mill Test Certificates documenting mechanical tensile properties, yield thresholds, elongation percentages, and chemical spectral analyses.
Manufacturing Supremacy
The Shenzhen Precision Hardware Ecosystem Advantage
Shenzhen and the Pearl River Delta represent the world's most concentrated precision industrial cluster. By anchoring our manufacturing base in Longgang, Shenzhen, Sunmy Hardware provides overseas clients with strategic procurement advantages that standalone Western machine shops cannot mirror.
Hyper-Localized Supply Infrastructure
Within a 25-kilometer radius, our facility accesses raw billet extrusion mills, specialized heat-treatment plants (vacuum quenching, cryogenics), and high-spec surface finishing lines (Type III hard anodizing, micro-arc oxidation, electroless nickel plating). This eliminates multi-week domestic transit delays.
Dynamic Scalability & Bridge Tooling
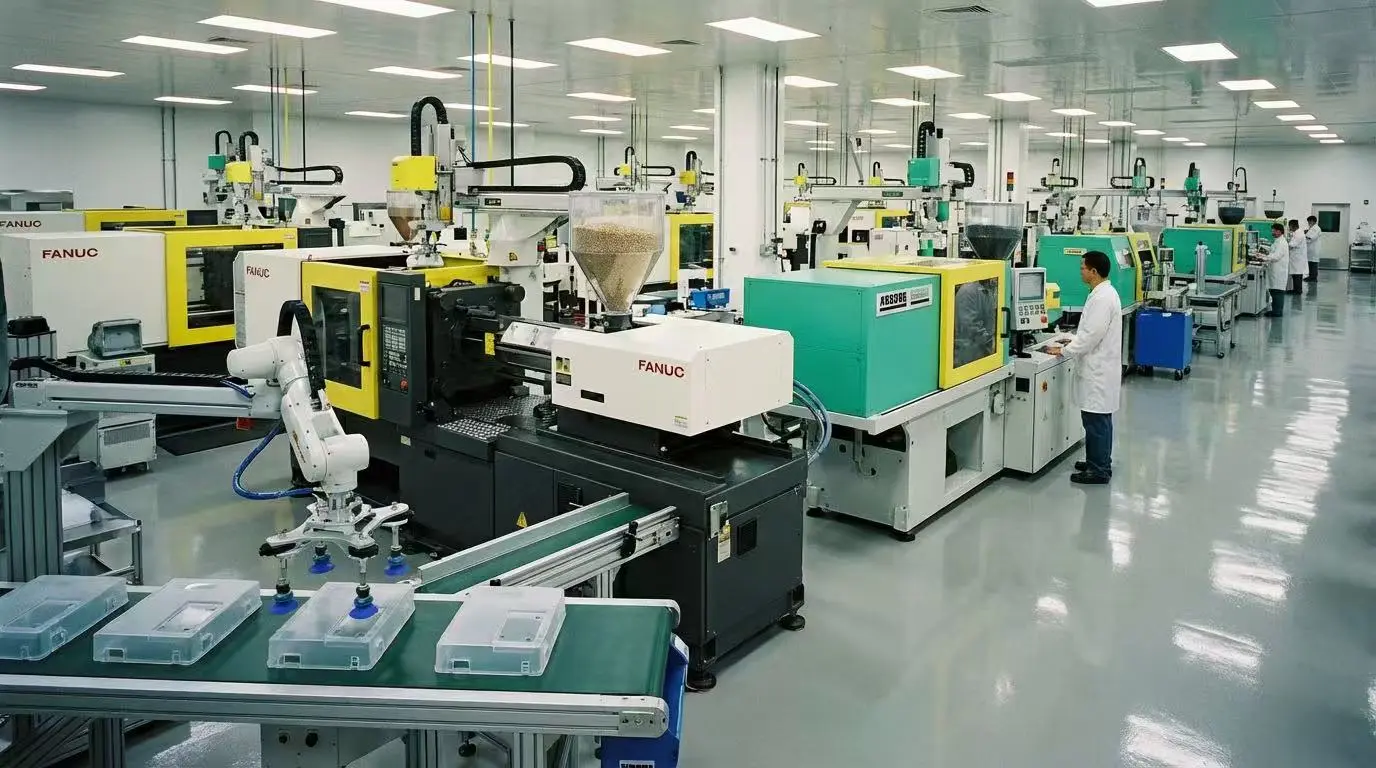
Whether your brand requires 25 prototype billet rearsets for dynamic track testing or a recurring production batch of 10,000 wheel spacers, our hybrid plant infrastructure bridges high-mix low-volume CNC machining directly into automated multi-spindle turning and high-pressure die casting without switching vendors.
Direct Engineering Collaboration
Trading companies introduce communication bottlenecks, IP vulnerability, and marked-up pricing. At Sunmy Hardware, global procurement teams collaborate directly with our senior manufacturing engineers. We dissect GD&T callouts, evaluate cutter radiuses, and deliver comprehensive DFM feedback in under 24 hours.
±0.005mm
Micro-Precision CNC Tolerance
5,000T/Yr
Annual Metal Processing Capacity
24Hrs
DFM Analysis & Quote Turnaround
100%
In-House CMM & FAI Verification
Subsystem Integration
High-Stress Application Scenarios for CNC Motorcycle Hardware
Motorcycle engineering balances unyielding structural strength with aggressive weight reduction. Here is how our custom CNC machining capabilities are deployed across critical motorcycle subsystems.
Front Fork Triple Clamps & Riser Yokes
Upper and lower triple tree clamps govern steering geometry, rake angle stability, and torsional compliance under heavy threshold braking. Machined from solid aerospace billet AL7075-T651, our yokes feature pocketed webbing to eliminate weight while maintaining rigidity to prevent fork stiction during hard cornering entry.
Radial Monobloc Brake Caliper Bodies
Hydraulic brake calipers experience extreme internal pressures (exceeding 100 bar) combined with radiant heat over 300°C from sintered pads. We mill single-piece monobloc calipers featuring internal cross-drilled fluid passages, micron-accurate piston bore honing, and titanium bleed nipple ports to eliminate pedal sponginess.
Adjustable Racing Rearset Assemblies
Ergonomic foot control systems require fine-pitch knurled pegs for boot grip, smooth dual ball-bearing pivot linkages for rapid gear engagement, and eccentric positioning brackets. Precision CNC milling ensures backlash-free shifting action and breakaway shear grooves that protect the master cylinder during track falls.
Lightweight Cush-Drive Wheel Hubs & Sprockets
Rotating unsprung mass dramatically impairs gyroscopic flickability and suspension response. Our CNC turned-milled wheel hubs utilize internally lightened 6061-T6 spools with integrated elastomer cush-drive dampening pockets and hard-anodized 7075-T6 drive sprockets with mud-clearing tooth profiles.
Electric Motorcycle (E-Moto) Powertrain Housings
The electrification of powersports demands CNC-machined liquid-cooled stator casings, inverter heatsinks with micro-channel fin arrays, and high-voltage busbar connectors. We mill complex sealed enclosures achieving IP67/IP69K ingress protection ratings with automated sealing groove profiling.
Suspension Swingarm Linkage & Rocker Arms
Progressive rear shock linkages translate wheel travel into spring compression. Sunmy Hardware manufactures high-load rocker arms with tight needle-bearing press-fit tolerances (H7 fit), guaranteeing zero axial play and buttery progressive damping curve characteristics over million-cycle lifespans.
Material Engineering Specs
Motorcycle CNC Machining Materials & Processing Matrix
A comprehensive technical breakdown of raw alloy selection, metallurgical yield parameters, achievable machining tolerances, and surface treatments engineered specifically for high-stress motorcycle subsystems.
| Material Grade | Tensile / Yield Strength | Critical Tolerances | Primary Motorcycle Applications | Recommended Surface Finish |
|---|---|---|---|---|
| AL6061-T6 Billet | Tensile: 310 MPa Yield: 276 MPa |
±0.010 mm (±0.0004 in) |
Engine cases, stator covers, bracketry, reservoir caps, fluid fittings | Type II Anodize (Clear/Color), Bead Blasting (120# Grit), Polished Chrome Look |
| AL7075-T651 Aerospace | Tensile: 572 MPa Yield: 503 MPa |
±0.005 mm (±0.0002 in) |
Triple clamps, clip-on tubes, rear sets, rear drive sprockets, swingarm pivots | Mil-A-8625 Type III Hardcoat Anodizing (50µm depth), PTFE Impregnation |
| Titanium Ti-6Al-4V (Grade 5) | Tensile: 950 MPa Yield: 880 MPa |
±0.008 mm (±0.0003 in) |
Wheel axles, swingarm pivot bolts, caliper mounting hardware, exhaust flanges | PVD Nitride (Burnished Rainbow / Burnt Blue / DLC Diamond Carbon), Vapor Honed |
| AISI 4140 Chromoly Steel | Tensile: 655 MPa Yield: 415 MPa |
±0.005 mm (±0.0002 in) |
Transmission shafts, internal gears, steering stems, high-shear axles | Gas Nitriding, QPQ Liquid Ferritic Nitrocarburizing, Black Oxide, Case Hardening |
| Stainless Steel 316L / 17-4 PH | Tensile: 1100 MPa (17-4 H900) Yield: 1000 MPa |
±0.005 mm (±0.0002 in) |
Brake rotor carrier buttons, hydraulic banjo bolts, exhaust header bungs | Electropolishing, ASTM A967 Chemical Passivation, Precision Centrifugal Deburring |
| Polyoxymethylene (Delrin / POM) | Tensile: 70 MPa Flexural: 98 MPa |
±0.020 mm (±0.0008 in) |
Frame sliders, bar-end weights, axle bobbins, internal cable guides | As-machined clean tool finish, cryogenic flash deburring, smooth satin |
Future-Ready Engineering
Global Procurement Trends & Next-Gen Motorcycle Machining
The motorcycle industry is currently traversing an era of rapid technological inflection. B2B buyers from OEM tiers to bespoke custom houses require manufacturing partners that anticipate the shifting technical landscape.
AI Generative Design & Topology Optimization
Weight reduction is no longer achieved by simple manual pocketing. Global aftermarket brands now utilize FEA generative algorithms to strip non-critical mass, resulting in organic, bone-like stress-lattice structural geometries. Machining these complex load paths requires sophisticated CAM multi-axis continuous swarf cutting and collision avoidance algorithms.
Supply Chain Resiliency & Dual Sourcing
Post-pandemic procurement strategies prioritize agile suppliers that reduce holding costs. Overseas OEMs increasingly partner with direct-export manufacturers capable of maintaining Kanban buffer inventory in bonded Shenzhen warehouses, supporting rapid release shipments to European and American assembly hubs within 48 to 72 hours.
Demand for Clean Aesthetic Surface Finishes
Exposed motorcycle parts are luxury visual centerpieces. Buyers now reject parts with visible tool chatter or uneven anodize rack marks. We employ diamond-tipped mono-crystalline milling inserts, automated 6-axis robotic polishing, and computerized multi-tank anodizing lines to achieve uniform deep-luster satin finishes.
Standard Operating Procedure
5-Stage Quality Assurance & Project Workflow
A systematic, transparent process engineered to protect your intellectual property, optimize part manufacturability, and eliminate dimensional deviations before international shipment.
01
Mutual NDA & CAD Onboarding
Bilateral non-disclosure executed before file transfer. Direct transfer of native STEP, IGES, Parasolid, and 2D GD&T drawings.
02
DFM & Tooling Simulation
Senior machinists analyze draft angles, cutter radiuses, wall thinness, and thermal warping risks within 24 hours.
03
Pilot FAI & Metrology
Pre-production sample run measured on Zeiss CMM. Complete First Article Inspection (FAI) report submitted for sign-off.
04
Full CNC Production
Batch manufacturing under statistical process control (SPC). In-process coordinate gauging and optical thread validation.
05
Export Packaging & Logistics
Custom foam-nesting, corrosion-inhibiting VCI bagging, wooden crating, and direct DDP/FOB ocean/air customs clearance.
Proven Track Record
Engineering Case Studies: Challenge, Solution, Result
Real-world examples of how Sunmy Hardware resolves complex manufacturing, tolerance, and structural failures for international OEMs.
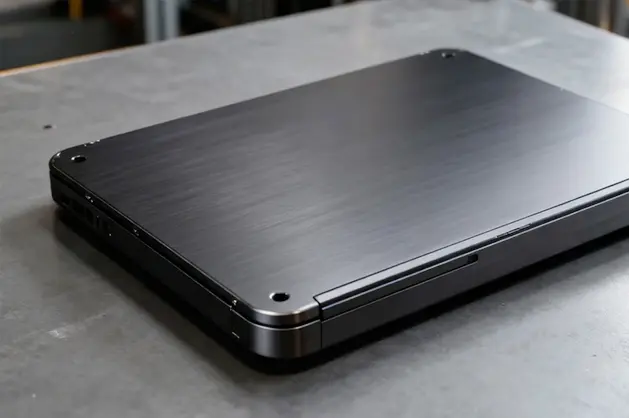
Case CS-MOTO-01 · Superbike Suspension
Request Technical Case Study
AL7075-T6 Billet Triple Clamp Fork Stiction Resolution
Challenge: An Italian racing team faced high-speed fork chatter and stiction under extreme corner braking. Their previous European machine shop experienced tool deflection, causing a 0.025 mm non-parallel taper across the dual 53 mm fork bore clamps.
Sunmy Solution: We re-engineered the toolpath strategy using dynamic trochoidal roughing and custom-ground carbide boring bars on our Hermle 5-axis center. We clamped both bores simultaneously, machining them in a single thermal envelope.
0.004 mm
Bore Parallelism
-18%
Weight via Webbing
Zero
Fork Stiction / Chatter
Case CS-MOTO-02 · High-Volume Powertrain
Discuss Your Casting Project
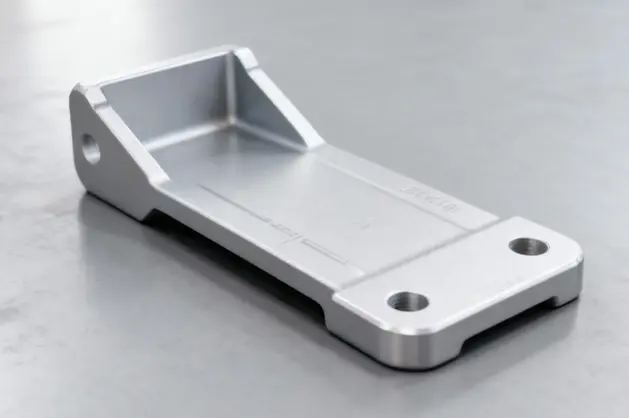
Vacuum Die-Cast + Post-CNC Engine Mount Bracket
Challenge: An American electric motorcycle manufacturer experienced sub-surface porosity during post-machining of their die-cast swingarm pivots, causing high-stress test fractures at 12,000 cycles.
Sunmy Solution: Redesigned runner gating via MAGMA moldflow analysis and shifted production to high-vacuum die casting. Implemented dedicated hydraulic clamping fixtures during secondary CNC milling to eliminate vibration-induced warpage.
-80%
Internal Porosity
100k+
Cycles Fatigue Life
100% Pass
Salt Spray & Shear Test
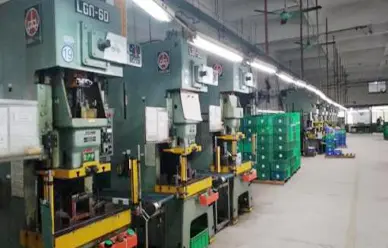
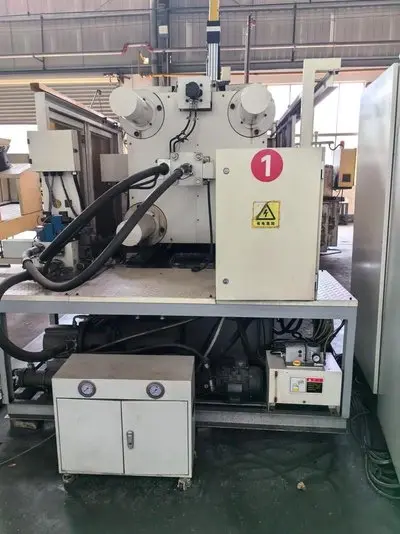
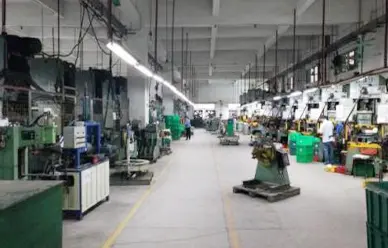
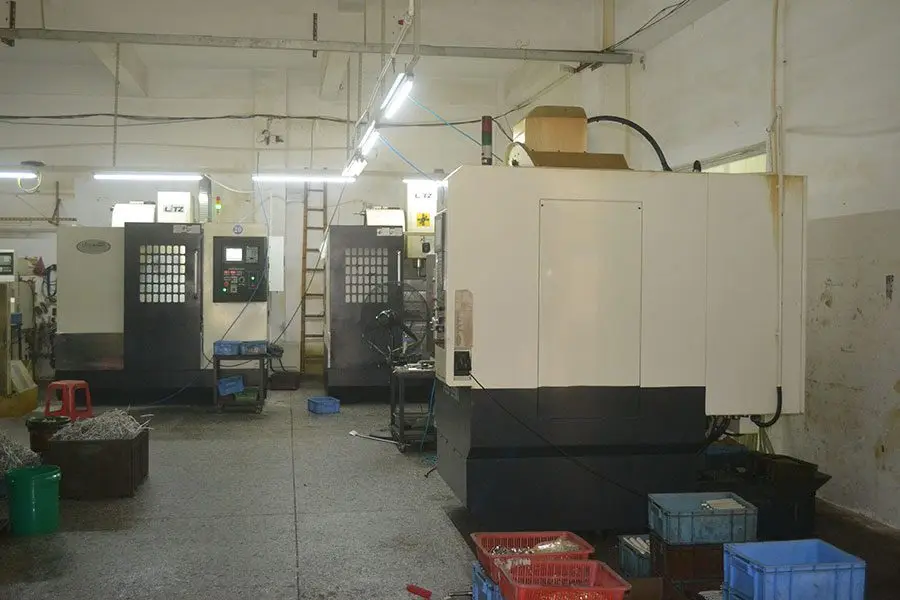
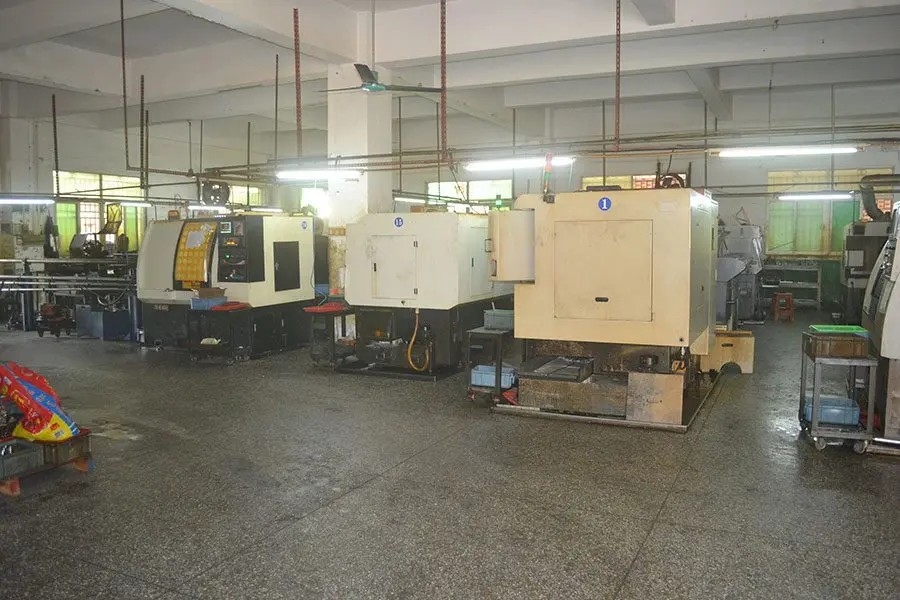
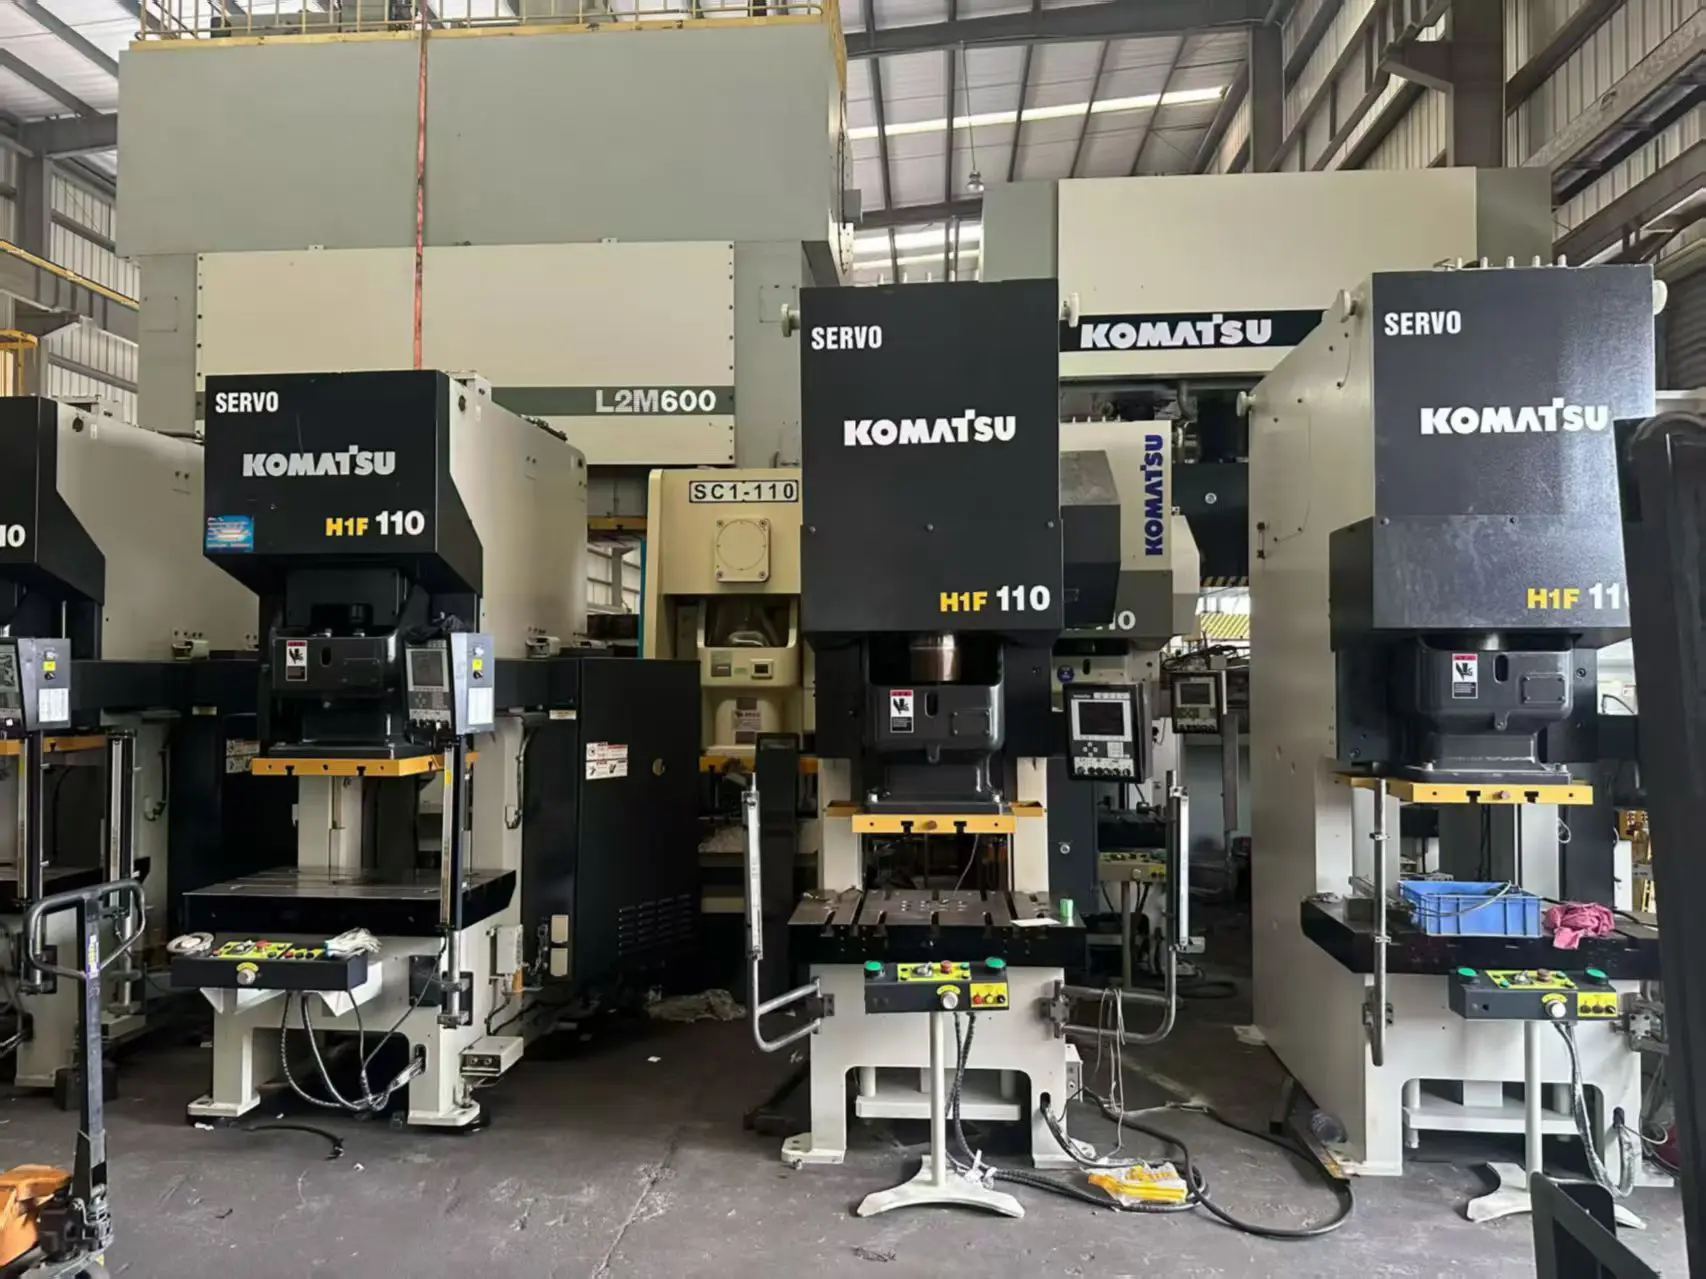
Shenzhen Production Base
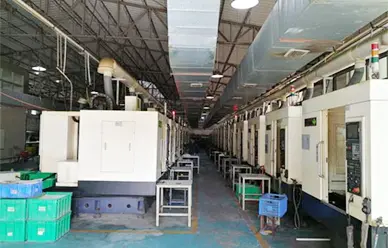
World-Class CNC Machinery & Metrology Center
Operating out of China South City (Huanancheng), Shenzhen since 2016, our facility is equipped with state-of-the-art multi-axis CNC milling, Swiss turning, and automated coordinate measuring machines (CMM).
Procurement Knowledge Base
Frequently Asked Questions: Sourcing Custom CNC Motorcycle Parts
In-depth technical answers addressing tolerance management, material certifications, testing regimes, and logistics for overseas procurement teams.
What tolerances can Sunmy hold on motorcycle safety components?
On critical bearing seats, shock rocker bores, and brake caliper piston cylinders, we reliably maintain tolerances down to ±0.005 mm (±0.0002 in). Standard CNC milled surfaces achieve ±0.01 mm to ±0.02 mm. Every critical dimension is validated in temperature-controlled inspection rooms using automated CMM tactile probes.
How do you guarantee material genuineness and avoid counterfeit alloys?
We source certified billets directly from audited domestic tier-1 aluminum mills (e.g., Chinalco and Southwest Aluminum). Each raw material batch is checked via in-house XRF spectroscopic chemical analyzers before cutting. Mill test reports according to EN 10204 3.1 with exact heat numbers are supplied with each export shipment.
How do you handle color consistency in multi-part anodized assemblies?
Motorcycle triple trees and rearsets frequently combine several sub-components that must exhibit identical visual color. We batch-anodize matching sets in a single immersion run using digitally controlled amperage, temperature (±1°C), and automated dye baths to ensure zero chromatic deviation across mating components.
How are proprietary CAD files and patented motorcycle designs protected?
We execute legally binding Non-Disclosure Agreements (NDAs) prior to receiving any 3D models or 2D blueprints. Sunmy Hardware operates an isolated internal engineering network where design files are encrypted and access is strictly restricted to designated project engineers. We never share customer designs with trading agents.
Can you assist with DFM optimization to reduce motorcycle part machining costs?
Yes. Over 80% of imported CAD models can achieve 15–30% machining cost reductions with minor geometry tweaks. Our engineers flag deep cavity radiuses requiring micro-tools, excessive setup re-clamping, unnecessary tight tolerances on non-mating cosmetic faces, and recommend standard cutter sizes during our free 24-hour DFM review.
What is your lead time for prototyping vs. full volume container shipments?
Rapid CNC prototypes in billet aluminum, titanium, or brass typically ship within 5 to 7 business days via DHL/FedEx Express. Production runs (500 to 10,000+ pieces) average 18 to 25 calendar days, including surface finishing and full CMM inspection. We also support scheduled blanket PO releases to balance client inventory flow.
Expanded Hardware Catalog
Precision Turned, Reducer & Structural Assemblies
Complementary precision-manufactured parts, knurled connectors, optical sleeves, and precision drone/robotic assemblies produced in our Shenzhen facility.








Direct Factory Engagement
Ready to Engineer Your Custom Motorcycle Parts?
Bypass trading intermediaries and collaborate directly with Shenzhen Sunmy Hardware's senior machining engineers. We review your STEP/IGES CAD geometry, assess GD&T feasibility, and submit competitive factory-direct quotations with comprehensive DFM feedback in under 24 hours.
Required Data for Instant RFQ:
- 3D CAD Models (.STEP, .STP, .IGES, or .X_T)
- 2D Blueprints with explicit GD&T & Tolerances (.PDF / .DWG)
- Alloy Grade & Surface Treatment Specification
- Batch Volumes (Prototypes vs. Recurring Production Runs)
Guaranteed Response Time: Within 24 Hours · Protected by Mutual NDA