
Precision Engineered Components & Cast Enclosures
Direct OEM manufacturing with micrometric dimensional repeatability, certified alloy chemistry, and 100% CMM inspection for Tier-1 supply chains.








High-Conductivity Alloy Selection & Cast Heat Sink Dynamics
Bridging the trade-off between fluid castability, dendrite grain spacing, and high thermal dissipation in mission-critical enclosures.
Alloy Heat Transfer Physics
Traditional structural casting alloys like A380 or ADC12 sacrifice thermal conductivity (approx. 96–113 W/m·K) to achieve high castability through silicon contents above 9%. Sunmy Hardware engineers low-iron, high-conductivity hyper-eutectic and silafont alloys (e.g., AlSi9Cu3, Al-CastK, and proprietary Al-Ni-Mg formulations) delivering 160–210 W/m·K while sustaining zero hot-tearing.
High-Pressure Die Casting (HPDC)
HPDC empowers intricate multi-fin thermal topologies with fin height-to-gap aspect ratios exceeding 12:1. Utilizing cold-chamber hydraulic injection machines from 280T to 3,500T with real-time multi-stage shot monitoring, our process prevents premature freezing in ultra-thin fin tips down to 0.8 mm thickness, reducing system weight by 35% compared to extruded alternatives.
Vacuum & Squeeze Casting
For liquid cold plates and IGBT power modules demanding leak-proof hermetic reliability, our vacuum-assisted die casting reduces gas entrapment porosity below ASTM E155 Grade 1. Squeeze casting applies sustained hydrostatic pressure during solidification, yielding weldable, heat-treatable (T5/T6) heat sink substrates with virtually zero micro-shrinkage.
| Alloy / Process Designation | Thermal Conductivity (W/m·K) | Tensile Yield Strength (MPa) | Max Fin Aspect Ratio | Porosity Defect Index (ASTM E155) | Primary Application Suitability |
|---|---|---|---|---|---|
| A380.0 / Traditional HPDC | 96 – 105 W/m·K | 160 MPa | 6 : 1 | Grade 3 – 4 | Consumer appliances, auxiliary enclosures |
| ADC12 / Standard Tooling | 100 – 115 W/m·K | 155 MPa | 8 : 1 | Grade 3 | Motor end-caps, generic LED heat sinks |
| AlSi10Mg(Fe) / Vacuum HPDC | 130 – 150 W/m·K | 180 MPa (T6) | 10 : 1 | Grade 1 – 2 | Automotive DC-DC converters, 5G RRU housings |
| ThermalAlloy-K (High Pure Al) | 185 – 210 W/m·K | 130 MPa | 14 : 1 | Grade 1 | AI Server cooling modules, GPU vapor chamber caps |
| A356 / Squeeze Casting | 165 – 175 W/m·K | 220 MPa (T6) | 11 : 1 | Near-Zero (Structural) | Liquid cold plate covers, traction inverter plates |
China Factory 4.0: Agile Supply Chains in the Greater Bay Area
Combining industrial clustering with real-time IoT metrology, closed-loop melt recycling, and frictionless engineering communication directly from Shenzhen.
Integrated Industrial Cluster
Situated in Shenzhen (Longgang District), Sunmy Hardware operates in the planetary epicenter of rapid prototyping and precision manufacturing. Tooling manufacture, core box fabrication, degassing flux refinement, and automated multi-axis deburring operate within a 30-kilometer logistics radius, cutting new die validation from 12 weeks to 22 business days.
Closed-Loop Circular Metallurgy
Industrial scale heat sink casting demands stringent sustainability. Our melting units integrate on-site spectrographic chemistry validation and argon rotor degassing to reuse 100% of runners, overflows, and trimmed alloy without introducing oxide inclusions, maintaining strict compliance with EU Carbon Border Adjustment Mechanisms (CBAM).
Direct Factory-to-Engineer Protocol
Intermediary traders dilute engineering nuance. At Sunmy, overseas mechanical and thermal engineers collaborate directly with our bilingual tooling designers and foundry masters. Every project starts with a comprehensive 24-hour DFM feedback report, mitigating thermal choke points before tool steel is cut.
Five Core Capabilities Under One Accountable Supplier
Eliminate multi-tier vendor risk by managing prototype CNC machining, volume die casting, stamping, and mold tooling under unified quality governance.
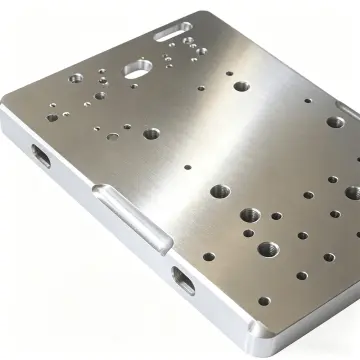
CNC Machining (In-House)
3, 4, and 5-axis milling plus mill-turn operations for high-density thermal mounting plates, sensor enclosures, and custom heat dissipation blocks held to ±0.005 mm precision.
Explore CNC Machining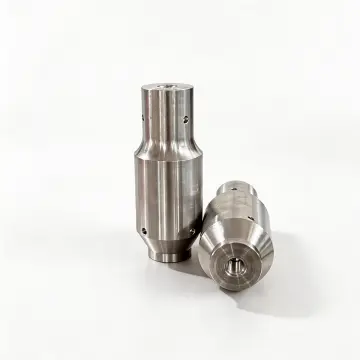
Precision Turned Parts
Swiss-type precision turning and high-speed CNC lathe production for brass thermal fittings, heat pipe connectors, core pins, bushings, and high-frequency RF contact probes.
Explore Turned Parts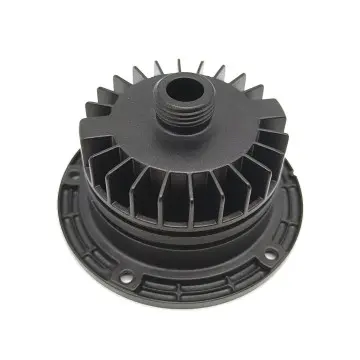
Die & Investment Casting
High-pressure aluminum and zinc die casting, low-pressure casting, and investment casting for heat sinks with complex geometric pin-fin topologies and low mass density.
Explore Castings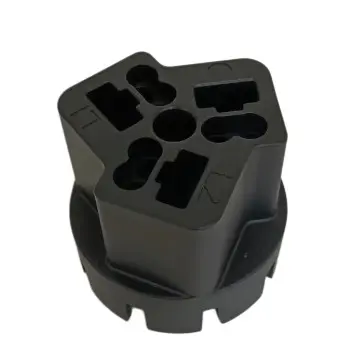
Plastic Injection Molding & Overmolding
Moldflow-backed injection molding for thermal insulator shrouds, connector terminal covers, cable carrier links, and flame-retardant (UL94-V0) electronic housings.
Explore Molding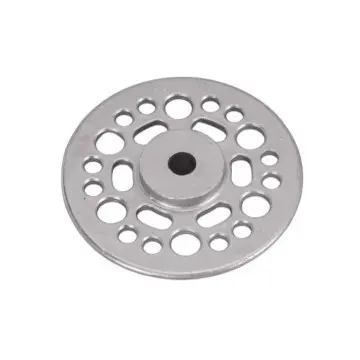
Sheet Metal Fabrication & Stamping (In-House)
Progressive die stamping, deep drawing, laser cutting, and folded-fin heat sink assemblies utilizing copper and electrical steel laminations for stator/rotor and battery busbars.
Explore StampingMacro-Industry Solutions for High-Heat Flux Electronics
Engineered heat sink castings tailored for demanding physical environments, galvanic resilience, and extreme vibrational fatigue resistance.
Electric Vehicles (EV)
Traction inverters, on-board chargers (OBC), and BMS enclosures require cast aluminum cold plates with internal serpentine fluid channels capable of withstanding 5.0 bar coolant pressure test cycles with zero leakage.
Hyperscale AI & HPC
GPU clusters and ASIC neural processors operating above 800W TDP require hybrid cast-and-vapor chamber thermal modules, combining thin-fin cast shrouds with copper baseplates to prevent semiconductor thermal throttling.
5G / 6G Massive MIMO
Remote Radio Units (RRU) installed on telecommunication towers endure unassisted natural convection. We cast high-aspect, self-cleaning flared fin enclosures tested to 1,000+ hours of ASTM B117 salt spray without corrosion degradation.
Energy Storage (BESS)
Utility-grade solar inverters and battery energy storage require large-envelope cast heat sinks delivering uniform temperature distributions (ΔT ≤ 2.5°C across battery module racks) to forestall cell degradation.
Heat Sink Casting Roadmap & Emerging Methodologies
Anticipating next-generation thermal challenges through generative design, micro-channel casting, and rheocasting techniques.
Semi-Solid Rheocasting (SSM)
Transitioning beyond liquid phase casting into thixotropic slurry states. Rheocasting allows the production of near-zero gas defect heat sink castings with globular microstructures, unlocking post-casting T6 solution heat treatment and anodizing color uniformity matching billet finishes.
AI-Generative Fin Morphologies
Replacing traditional parallel fin arrays with computational CFD topology optimization. Cast pin matrices designed via genetic algorithms feature non-linear, bio-inspired air pathways that generate localized boundary layer micro-vortices, amplifying heat transfer coefficients by 28% under forced convection.
Cast-In Tube & FSW Liquid Cold Plates
Integrating pre-formed stainless steel or OFHC copper cooling conduits directly inside the aluminum die casting die during the shot cycle. Friction Stir Welding (FSW) is deployed to hermetically seal cast fluid channels, guaranteeing zero fluid-circuit bypass at operating pressures up to 12 bar.
Engineering Case Studies: Defect Elimination & Yield Optimization
Real-world interventions where Sunmy Hardware resolved intractable thermal resistance, gas porosity, and geometric warpage issues for international OEMs.
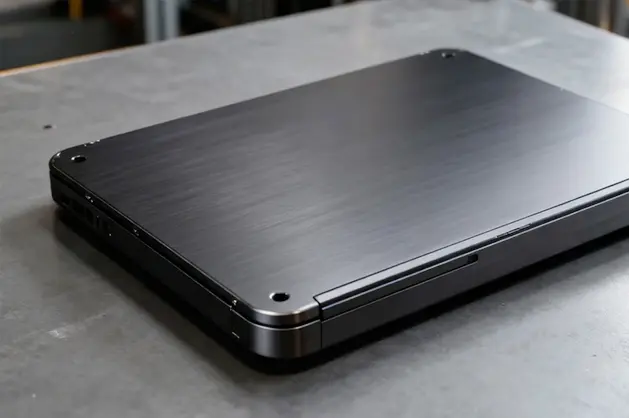
Aluminum Alloy Thermal Chassis & Shielding
The Engineering Bottleneck: A European IoT device brand suffered inconsistent mating between their system-on-chip (SoC) and their cast chassis. The prior manufacturer allowed thermal base warping of up to 0.18 mm, causing localized hotspot thermal shutdowns.
Sunmy's Intervention: Re-engineered the mold gate geometry, balanced runner feed pressure, and implemented custom multi-axis CNC skim-milling in dedicated pneumatic fixtures to hold mating surface planarity within 0.02 mm across the 180 mm span.
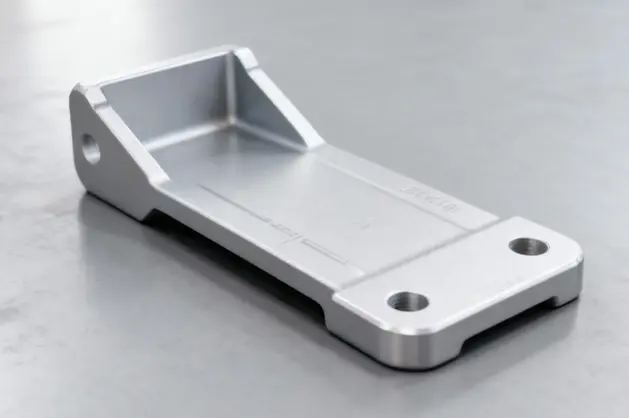
Die-Cast Vacuum Power Inverter Heat Sink
The Engineering Bottleneck: A Tier-1 automotive customer experienced failure during helium mass spectrometer leak tests on fluid-cooled motor controller plates due to sub-surface dendritic shrinkage pores.
Sunmy's Intervention: Deployed vacuum-assisted high-pressure die casting (evacuating the cavity to <50 mbar before shot entry), combined with conformal mold chill circuits to accelerate dendritic solidification in thick mounting bosses.
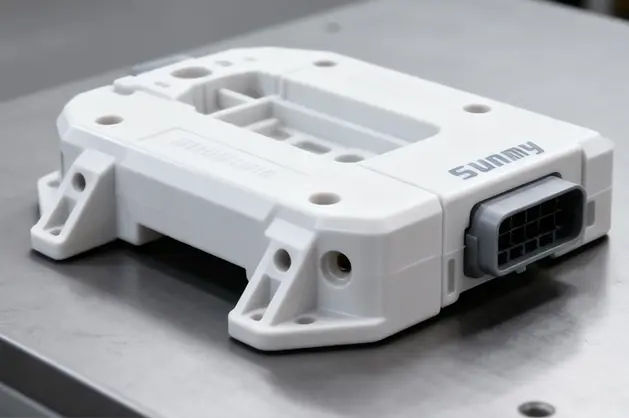
High-Duty Robotic Actuator Thermal Housing
The Engineering Bottleneck: Precision multi-axis joint servos produced rapid heat accumulation, degrading internal magnetic encoders. Extruded solutions lacked the mounting boss complexity needed for optical encoders.
Sunmy's Intervention: Developed a high-density radial fin cast housing with integral bearing seats, turn-milled in a single chucking setup to guarantee concentricity between motor air-gap and exterior cooling fins.
Full Regulatory Traceability & Metrology Verification
Empowering European and North American procurement teams with auditable metallographic, dimensional, and environmental compliance certifications.
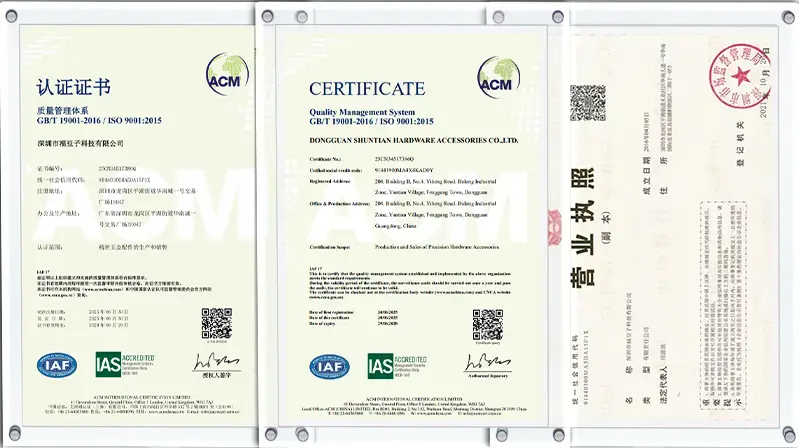
Standard Documentation Included with Every Production Lot:
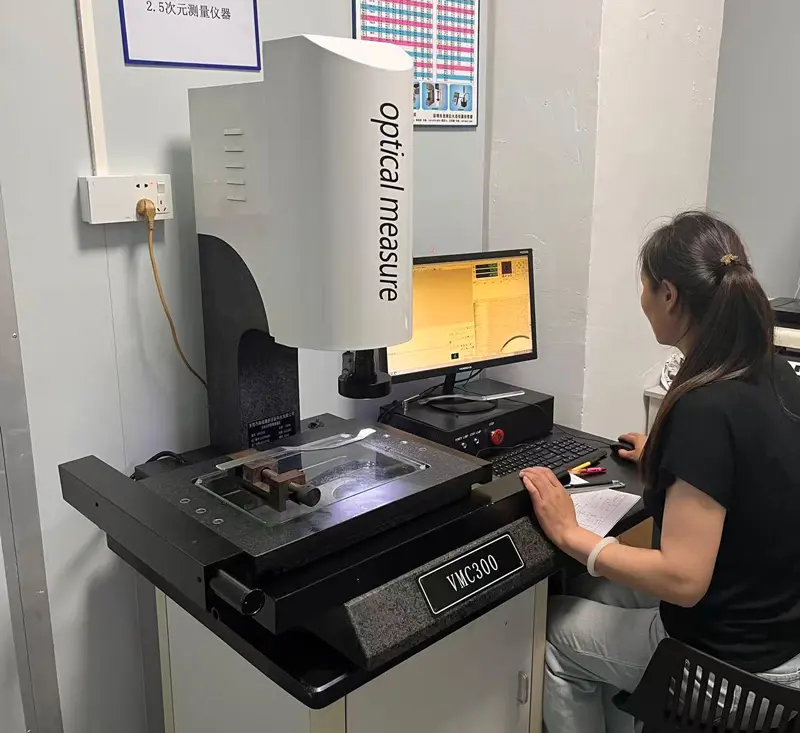
- Full CMM Metrology & FAI Reports: 3D coordinate measuring machines (CMM) record dimensional GD&T callouts, surface profile runout, and hole positional tolerances.
- Direct Spectrometric Melt Certifications: Optical emission spectroscopy (OES) reports detailing iron (Fe), copper (Cu), and silicon (Si) fractioning per ladle melt.
- RoHS, REACH & Conflict Minerals Statements: Mandatory declaration verifying total absence of hazardous heavy metals for compliant European and US importation.
- Non-Destructive Testing (NDT): Real-time industrial X-ray inspection for internal void validation and hydrostatic pressure testing for liquid-cooled plates.
Heat Sink Casting DFM Checklist for Global Buyers
Essential design guidelines to maximize thermal efficiency while reducing die wear and eliminating secondary machining costs.
1. Fin Draft Angle Optimization
Die-cast fins require a minimum draft angle of 0.5° to 1.5° per side to allow ejection without galling or bending. Using high-lubricity PVD tool coatings, Sunmy achieves draft angles as tight as 0.5°, maximizing fin surface area per unit volume.
2. Baseplate-to-Fin Transition
Abrupt cross-sectional steps create turbulent metal front flow and thermal bottlenecks. Radiused fillet transitions (R ≥ 1.0 mm) between the primary heat spreader plate and fin bases prevent hot tears during cooling and lower air pressure drop.
3. Secondary CNC Stock Allowance
To deliver mirror TIM planarity (<0.03 mm) without cutting into sub-surface porosity layers, specify 0.5 mm to 0.8 mm machining allowance on critical mounting faces. High-pressure skin contains minimal gas; excessive tool cuts must be avoided.
4. Ejector Pin Placement Strategy
Ejector pins must never impinge upon thermal contact zones or critical fluid gasket channels. Sunmy’s upfront tooling DFM maps all witness marks to non-functional perimeter flanges, protecting semiconductor thermal contact paths.
5. Anodizing vs. Conversion Coatings
Standard casting alloys with >3% silicon develop a dark mottled hue when hard anodized. For cosmetic consumer-facing housings, we formulate proprietary low-Si alloys or recommend trivalent chromate conversion (MIL-DTL-5541) for uninhibited thermal transfer.
6. Tooling Steel Selection & Life
Thermal fatigue cracking (heat checking) is the primary mode of die failure. We manufacture all high-stress heat sink cores from premium Bohler W300 or Dievar tool steels hardened to 46–50 HRC, assuring 100,000+ shots before re-tooling.
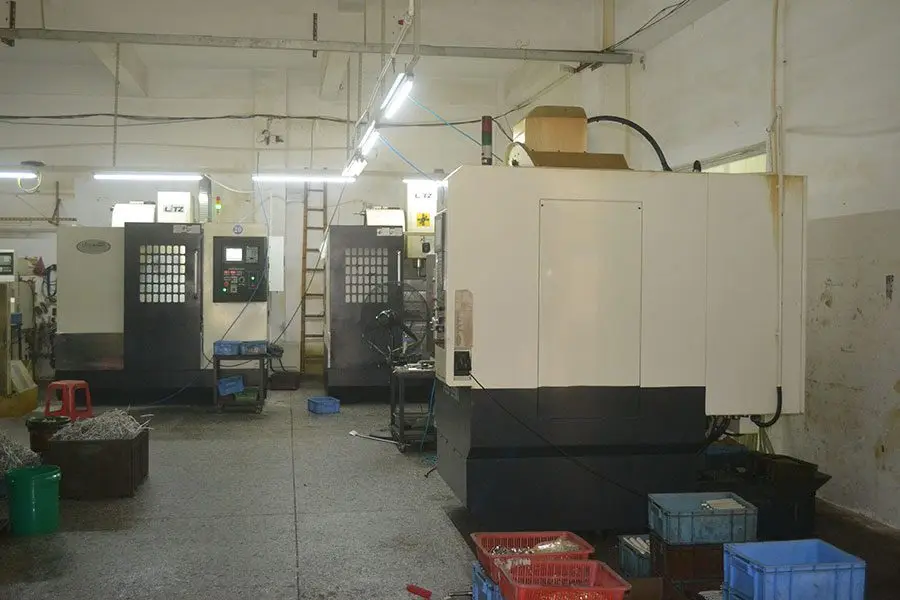
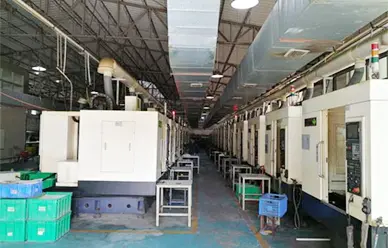
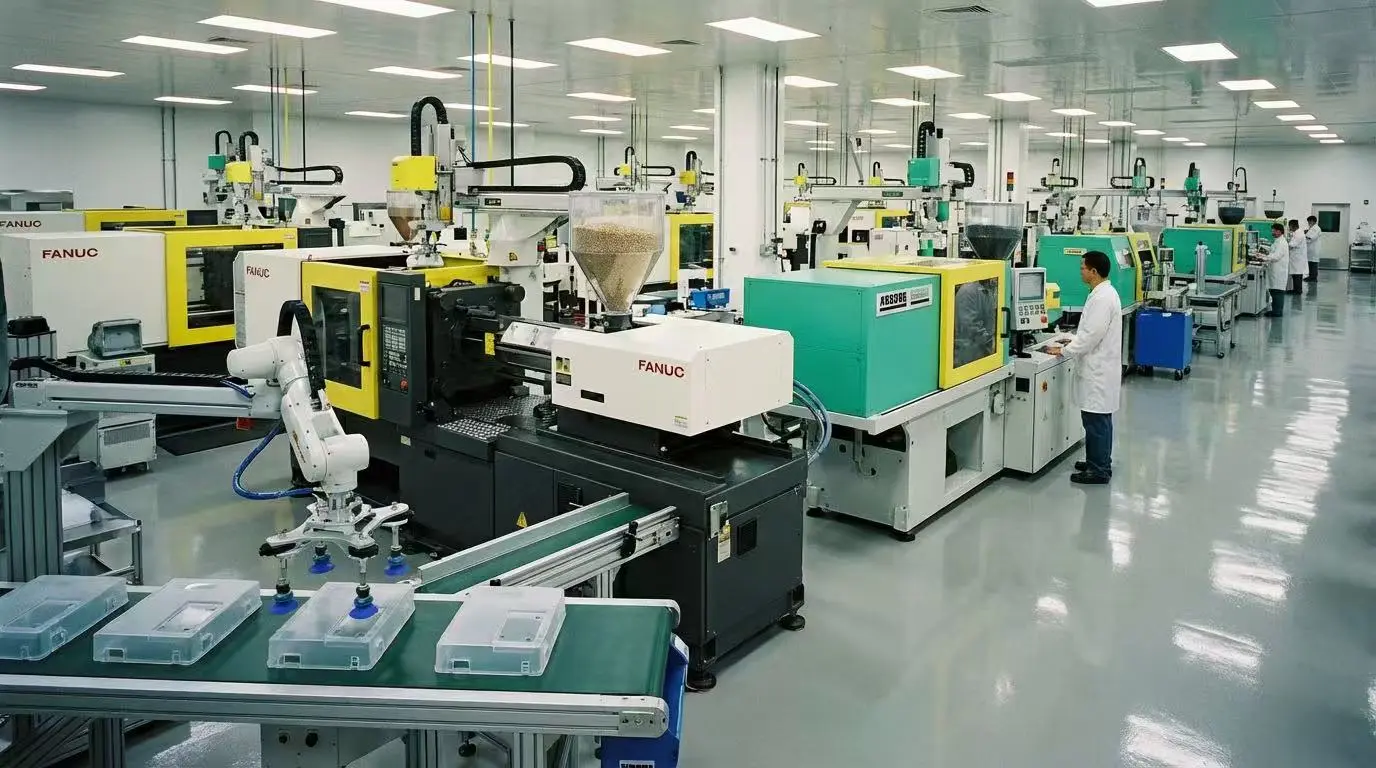
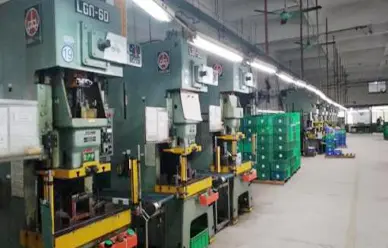
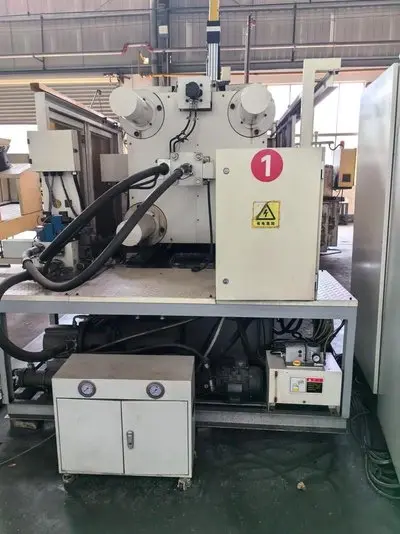
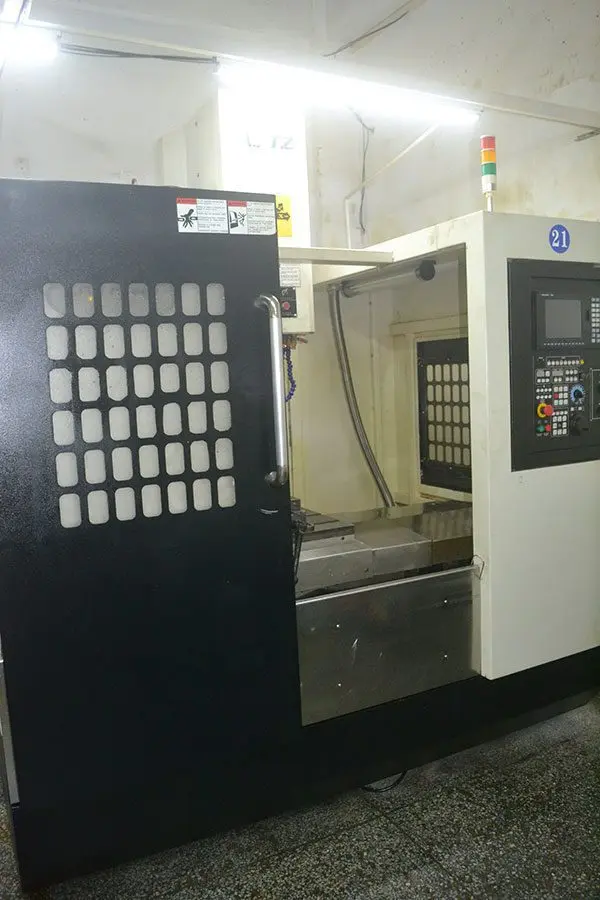
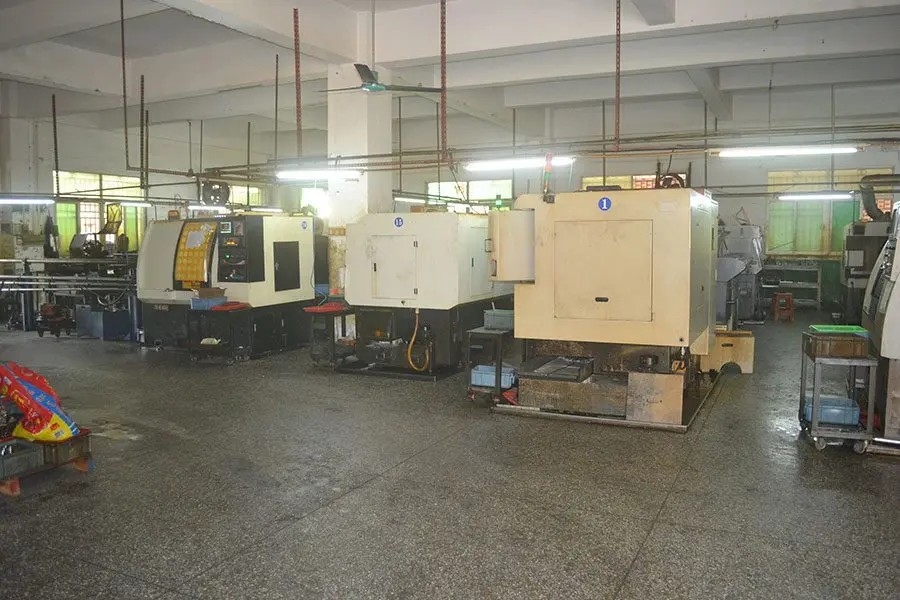
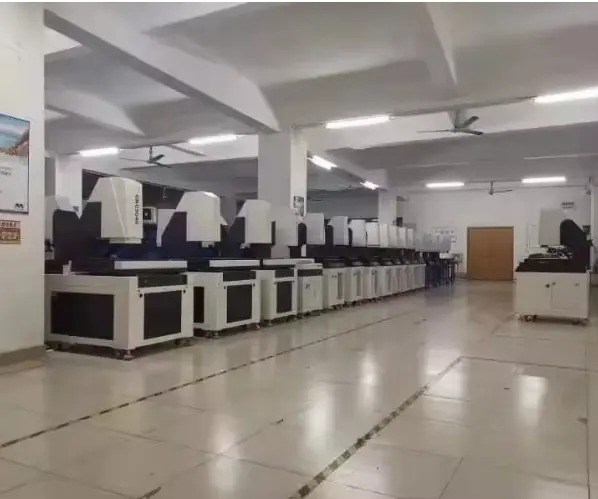
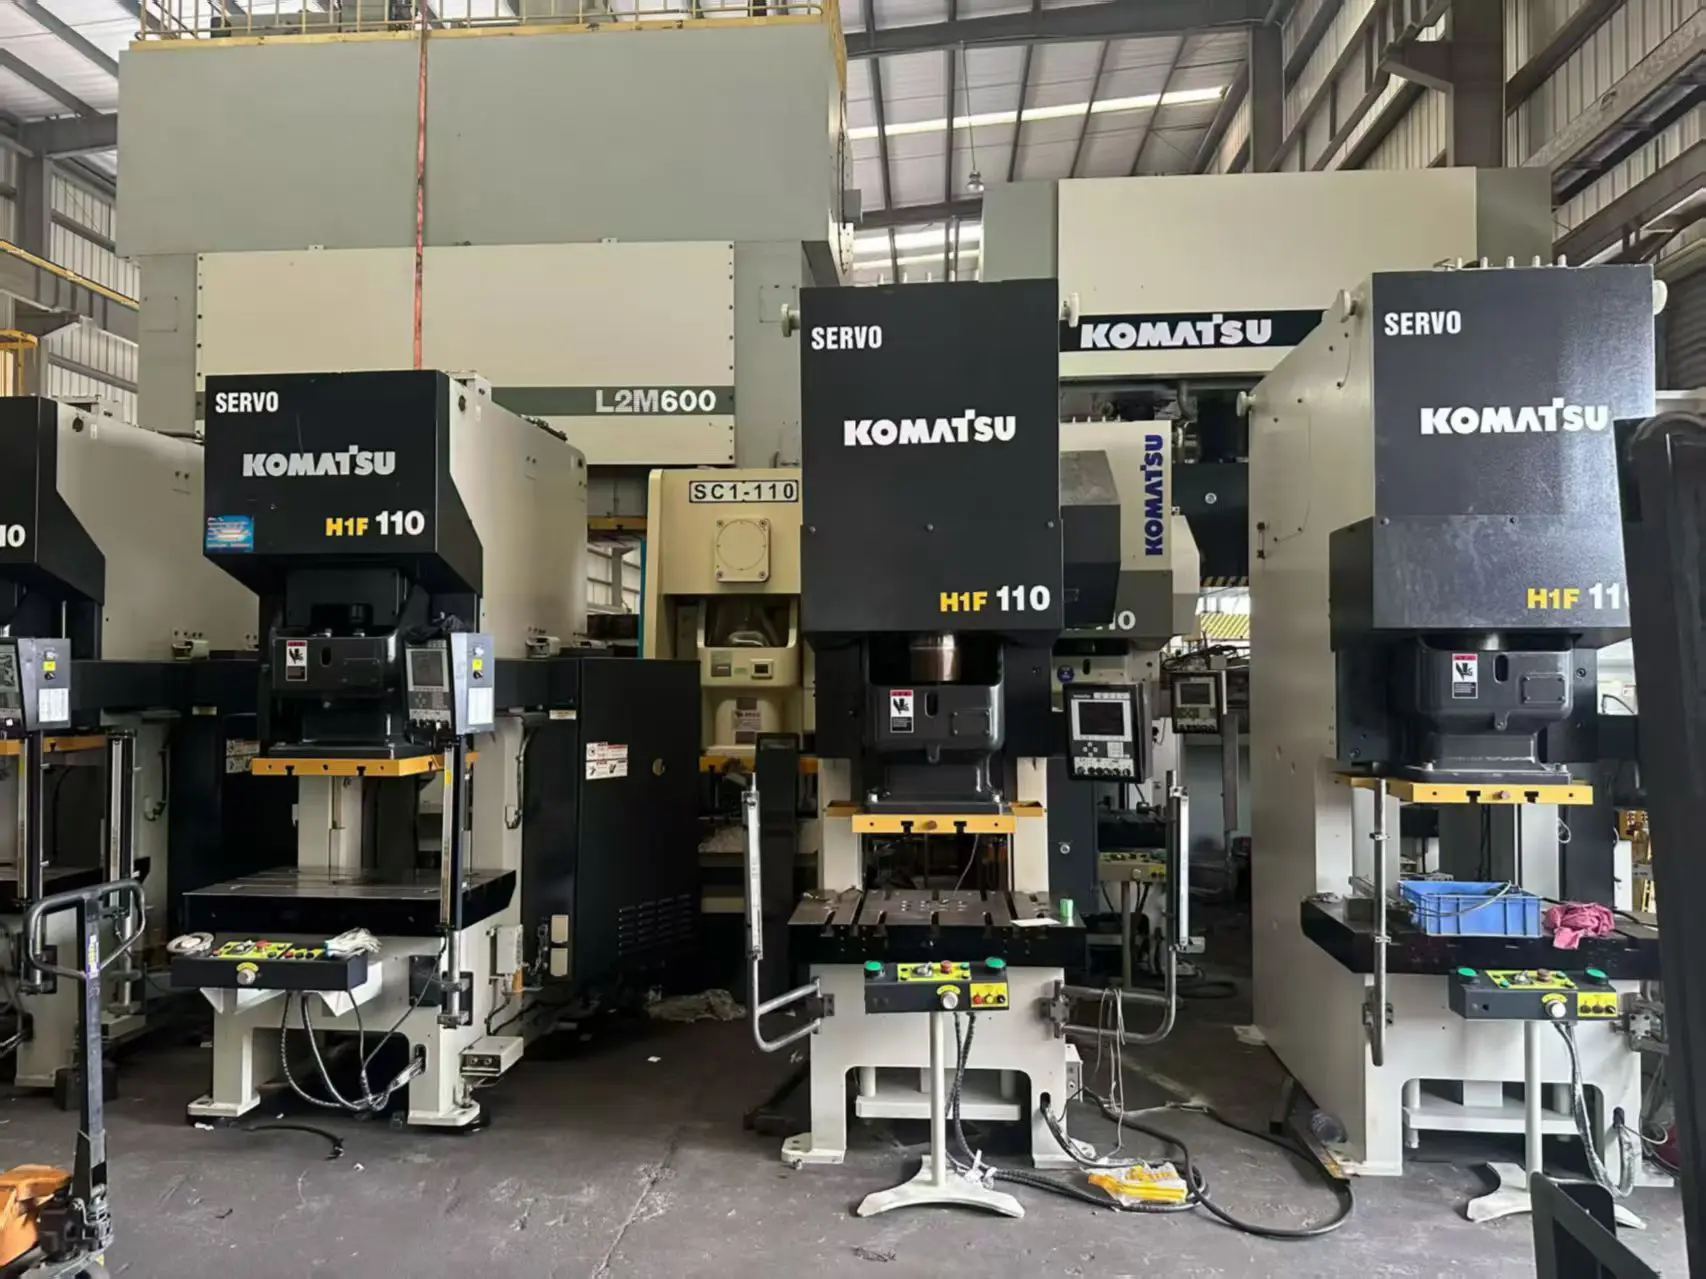
Precision Manufacturing & Quality Control Operations
A transparent look inside our Shenzhen production lines, automated CNC cells, and temperature-controlled metrology suites.
Advanced Precision Assemblies & Specialized Parts
From 5-axis aerospace impellers to knurled brass electronic connectors and flexible copper busbars.








Frequently Asked Questions on Heat Sink Casting & OEM Sourcing
Detailed technical answers addressing tolerances, tooling lifetime, thermal efficiency, and intellectual property safety.
What tolerances can Sunmy Hardware hold on die-cast and CNC-machined heat sinks?
How does die-cast thermal performance compare to extruded or skived heat sinks?
Which processes are manufactured in-house vs. partnered?
How does Sunmy protect 3D CAD data, patent files, and intellectual property?
What is the standard tooling life and lead time for high-pressure die casting dies?
How do you prevent porosity in liquid cold plates and sealed thermal housings?
Initiate Your Custom Heat Sink Casting Project
Send your 2D/3D technical drawings today. Our bilingual thermal metallurgists and tooling directors deliver an actionable DFM review, material selection guidance, and a transparent pricing quote within 24 hours.
Submit CAD / STEP Files
Direct factory upload under bilateral NDA protection